



Advanced In-House Production
All components and assembly operations are tightly controlled within a modern 40,000 sqm factory ensuring precision engineering and shorter time-to-market.
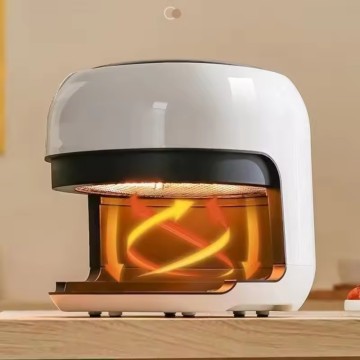 New Arrivals Large Capacity Deep Frying Pan Oven Visual Air Fryer
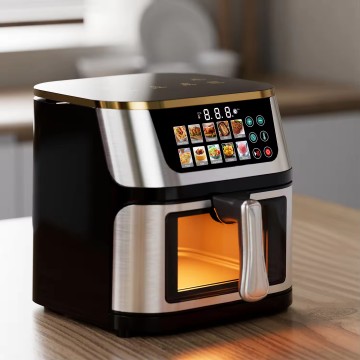 Air Fryer Oven Large Capacity 15L 10L 8L 6L 5L Digital Touch Smart Air Fryer With Glass Window for Home Kitchen
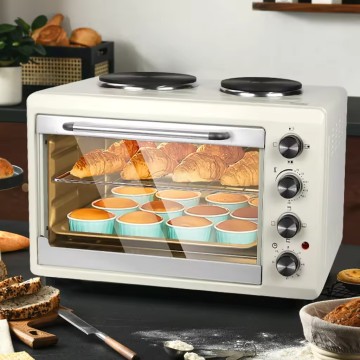 OEM Electric Oven for Baking Cake Bread Pizza Ovens 56L Kitchen Smart Home Toaster Oven
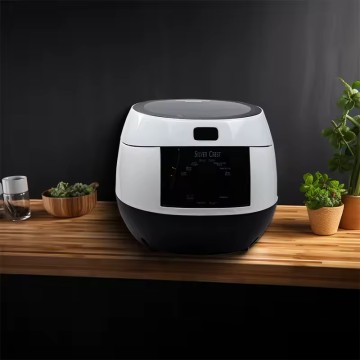 6L Smart Multi-function Automatic Electric Digital Keep Warm Crest Rice Cooker Support Customization
Electric microwave ovens have become an indispensable tool in the modern restaurant kitchen, especially for pre-processing tasks that streamline food preparation workflows. Designed for rapid heating and defrosting, these ovens enable chefs and kitchen staff to pre-cook, reheat, and partially prepare ingredients before final cooking and plating. This reduces wait times, enhances consistency in dishes, and increases operational efficiency in high-volume kitchens.
In busy commercial kitchens, where time is money and quality crucial, electric microwave ovens fill a vital niche. Their versatility allows for quick thawing of frozen products, melting ingredients like butter or chocolate, and even steaming vegetables or reheating sauces consistently without overcooking. This capability supports better inventory management by enabling batch pre-processing during off-peak hours, thus smoothing service peaks.
The commercial kitchen appliance market, particularly for electric microwave ovens designed for restaurant pre-processing, is experiencing robust growth driven by evolving foodservice trends and technology enhancements. Increasing demand for faster service, coupled with labor shortages in hospitality, drives automation and efficiency-focused equipment adoption.
Modern electric microwave ovens now often include programmable cycles, sensor cooking technologies, and energy-efficient components tailored to industrial-scale use. Suppliers increasingly integrate IoT-enabled features that allow predictive maintenance and remote monitoring, improving equipment uptime and reducing operational disruptions in restaurants, catering services, hotel kitchens, and institutional food programs.
Current trends in electric microwave ovens for restaurant pre-processing include multi-functionality and hybrid cooking methods combining microwave power with convection or grill elements. These advances allow operators to perform multiple cooking tasks with a single device, saving valuable kitchen space and reducing capital expenses.
Sustainability considerations are also shaping product design. Energy-efficient ovens with enhanced insulation reduce electricity consumption, while improved construction materials extend product lifespans and facilitate easier recycling at end-of-life. Further, the adoption of intuitive digital interfaces and AI-based cooking algorithms enhances ease of use and consistency, critical in busy, mixed-skill kitchens.
Specific applications for electric microwave ovens in restaurant pre-processing go beyond simple reheating:
Such varied uses highlight the electric microwave oven’s indispensable role as a flexible, time-saving appliance within commercial kitchens aiming for high throughput while maintaining culinary quality standards.
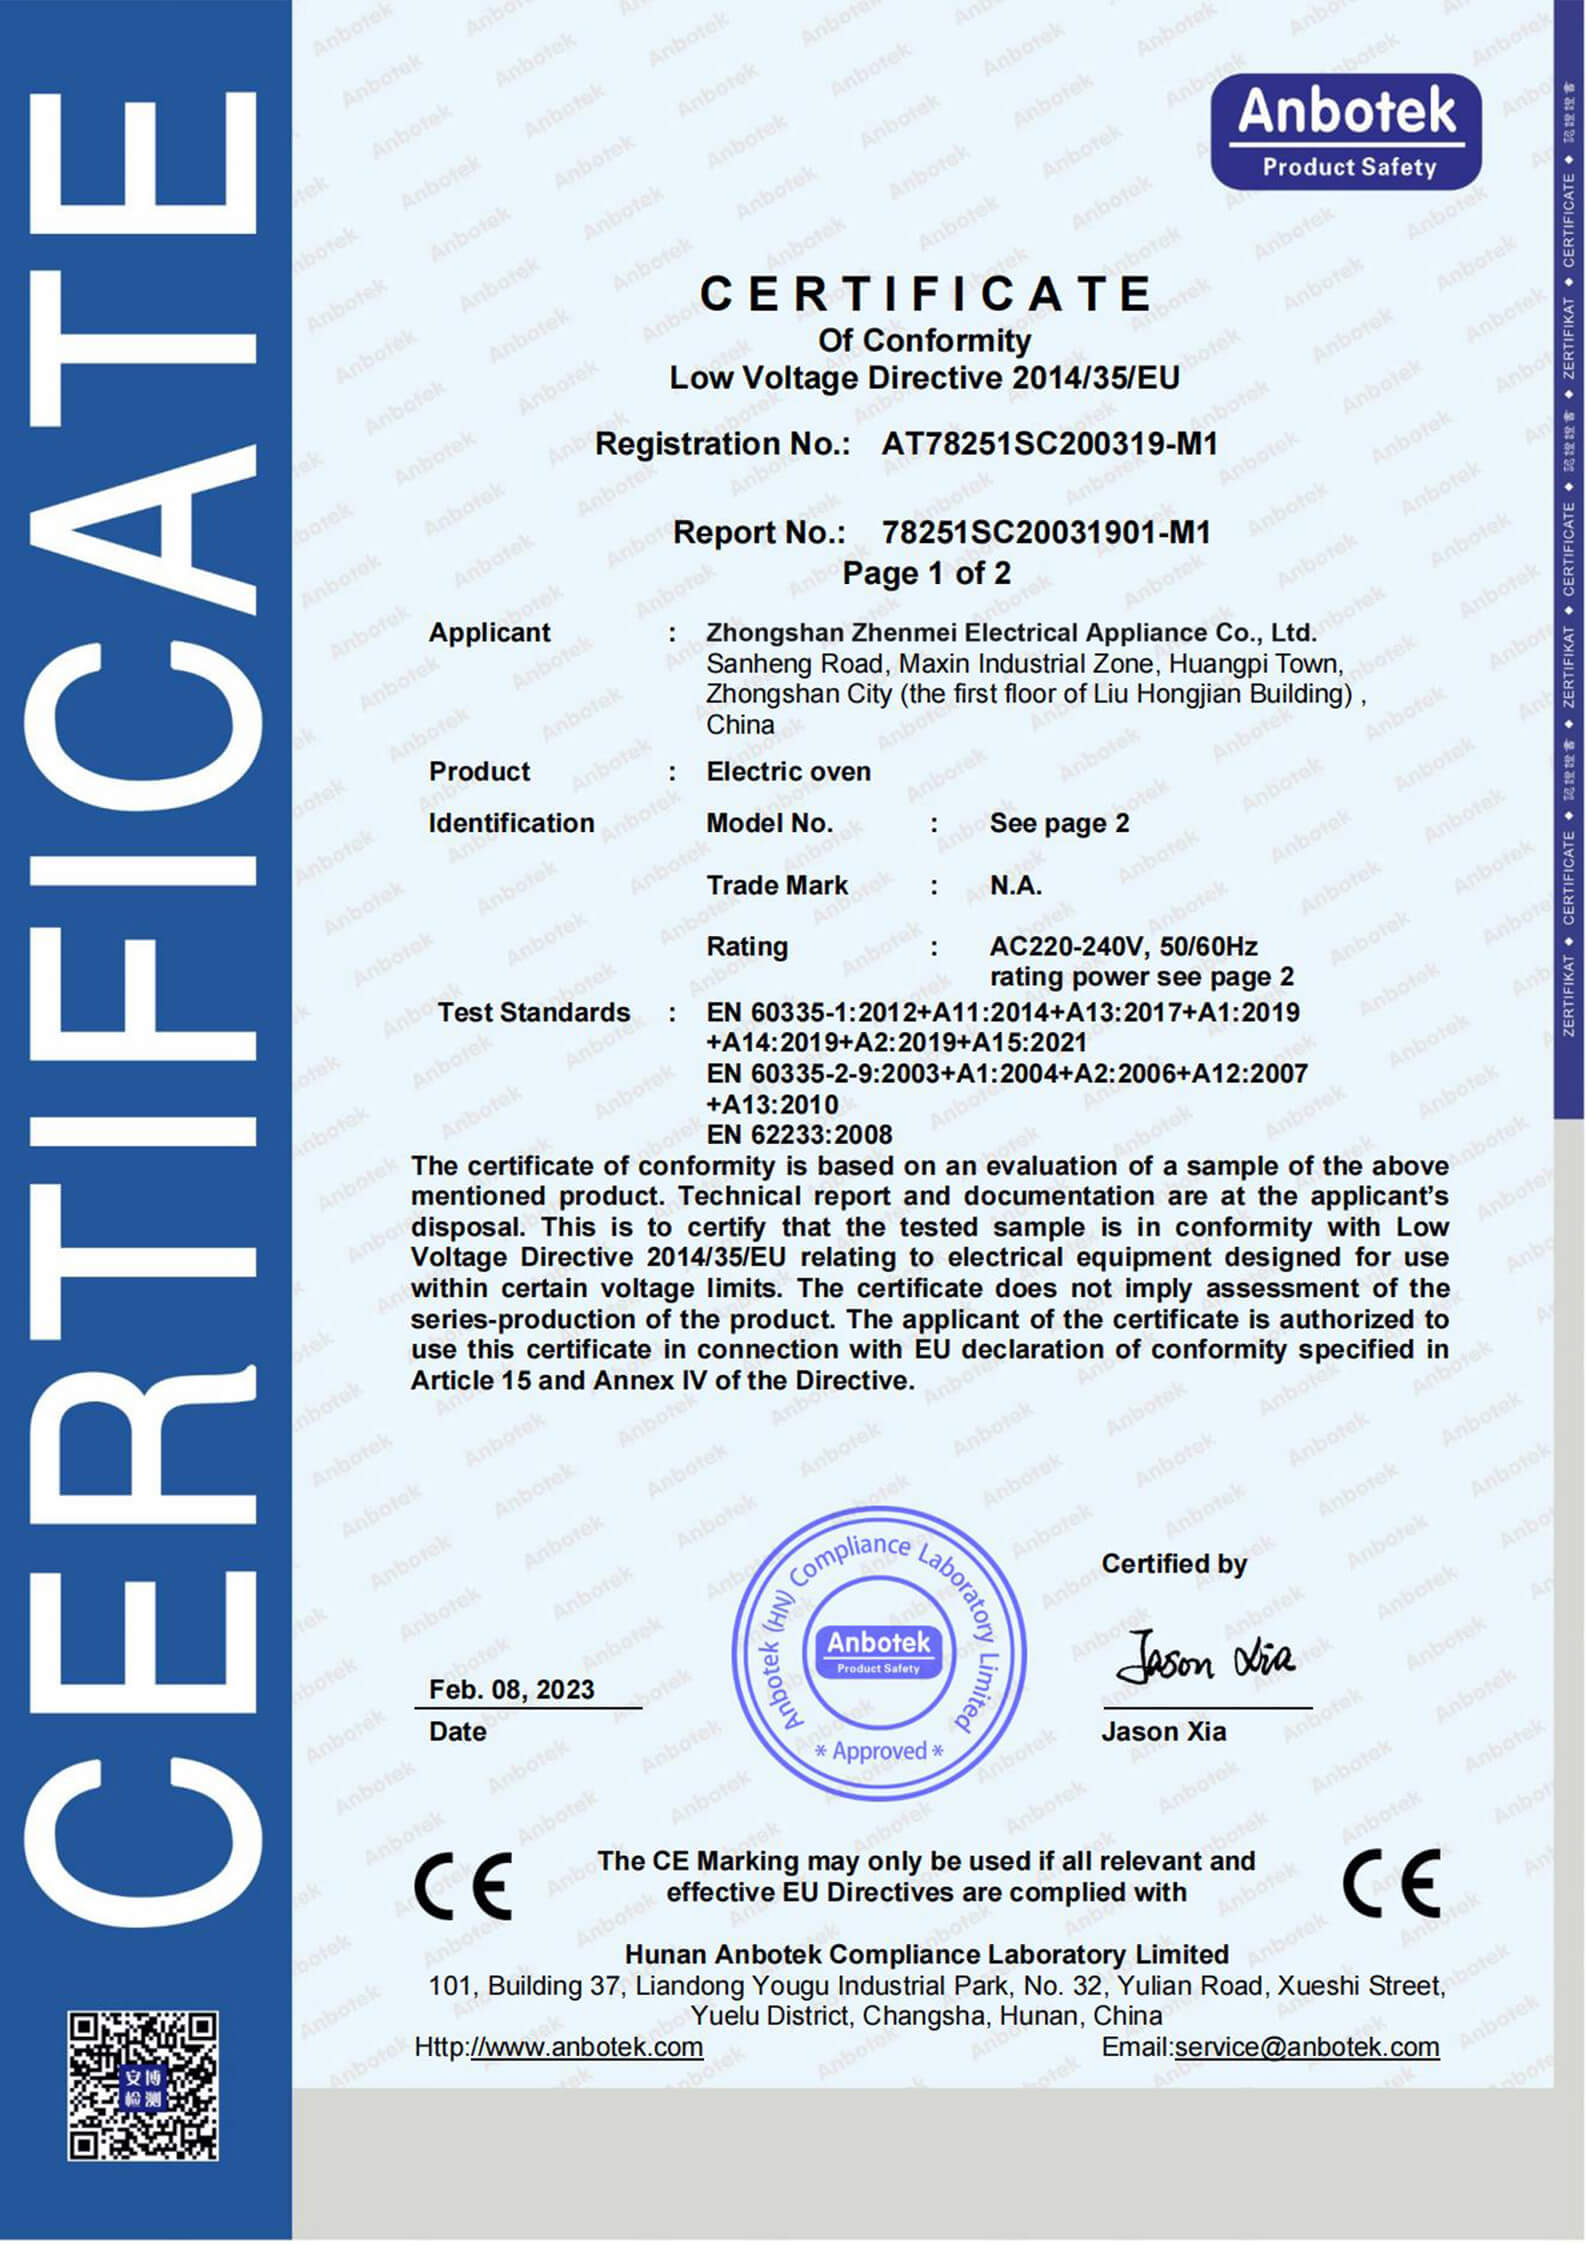
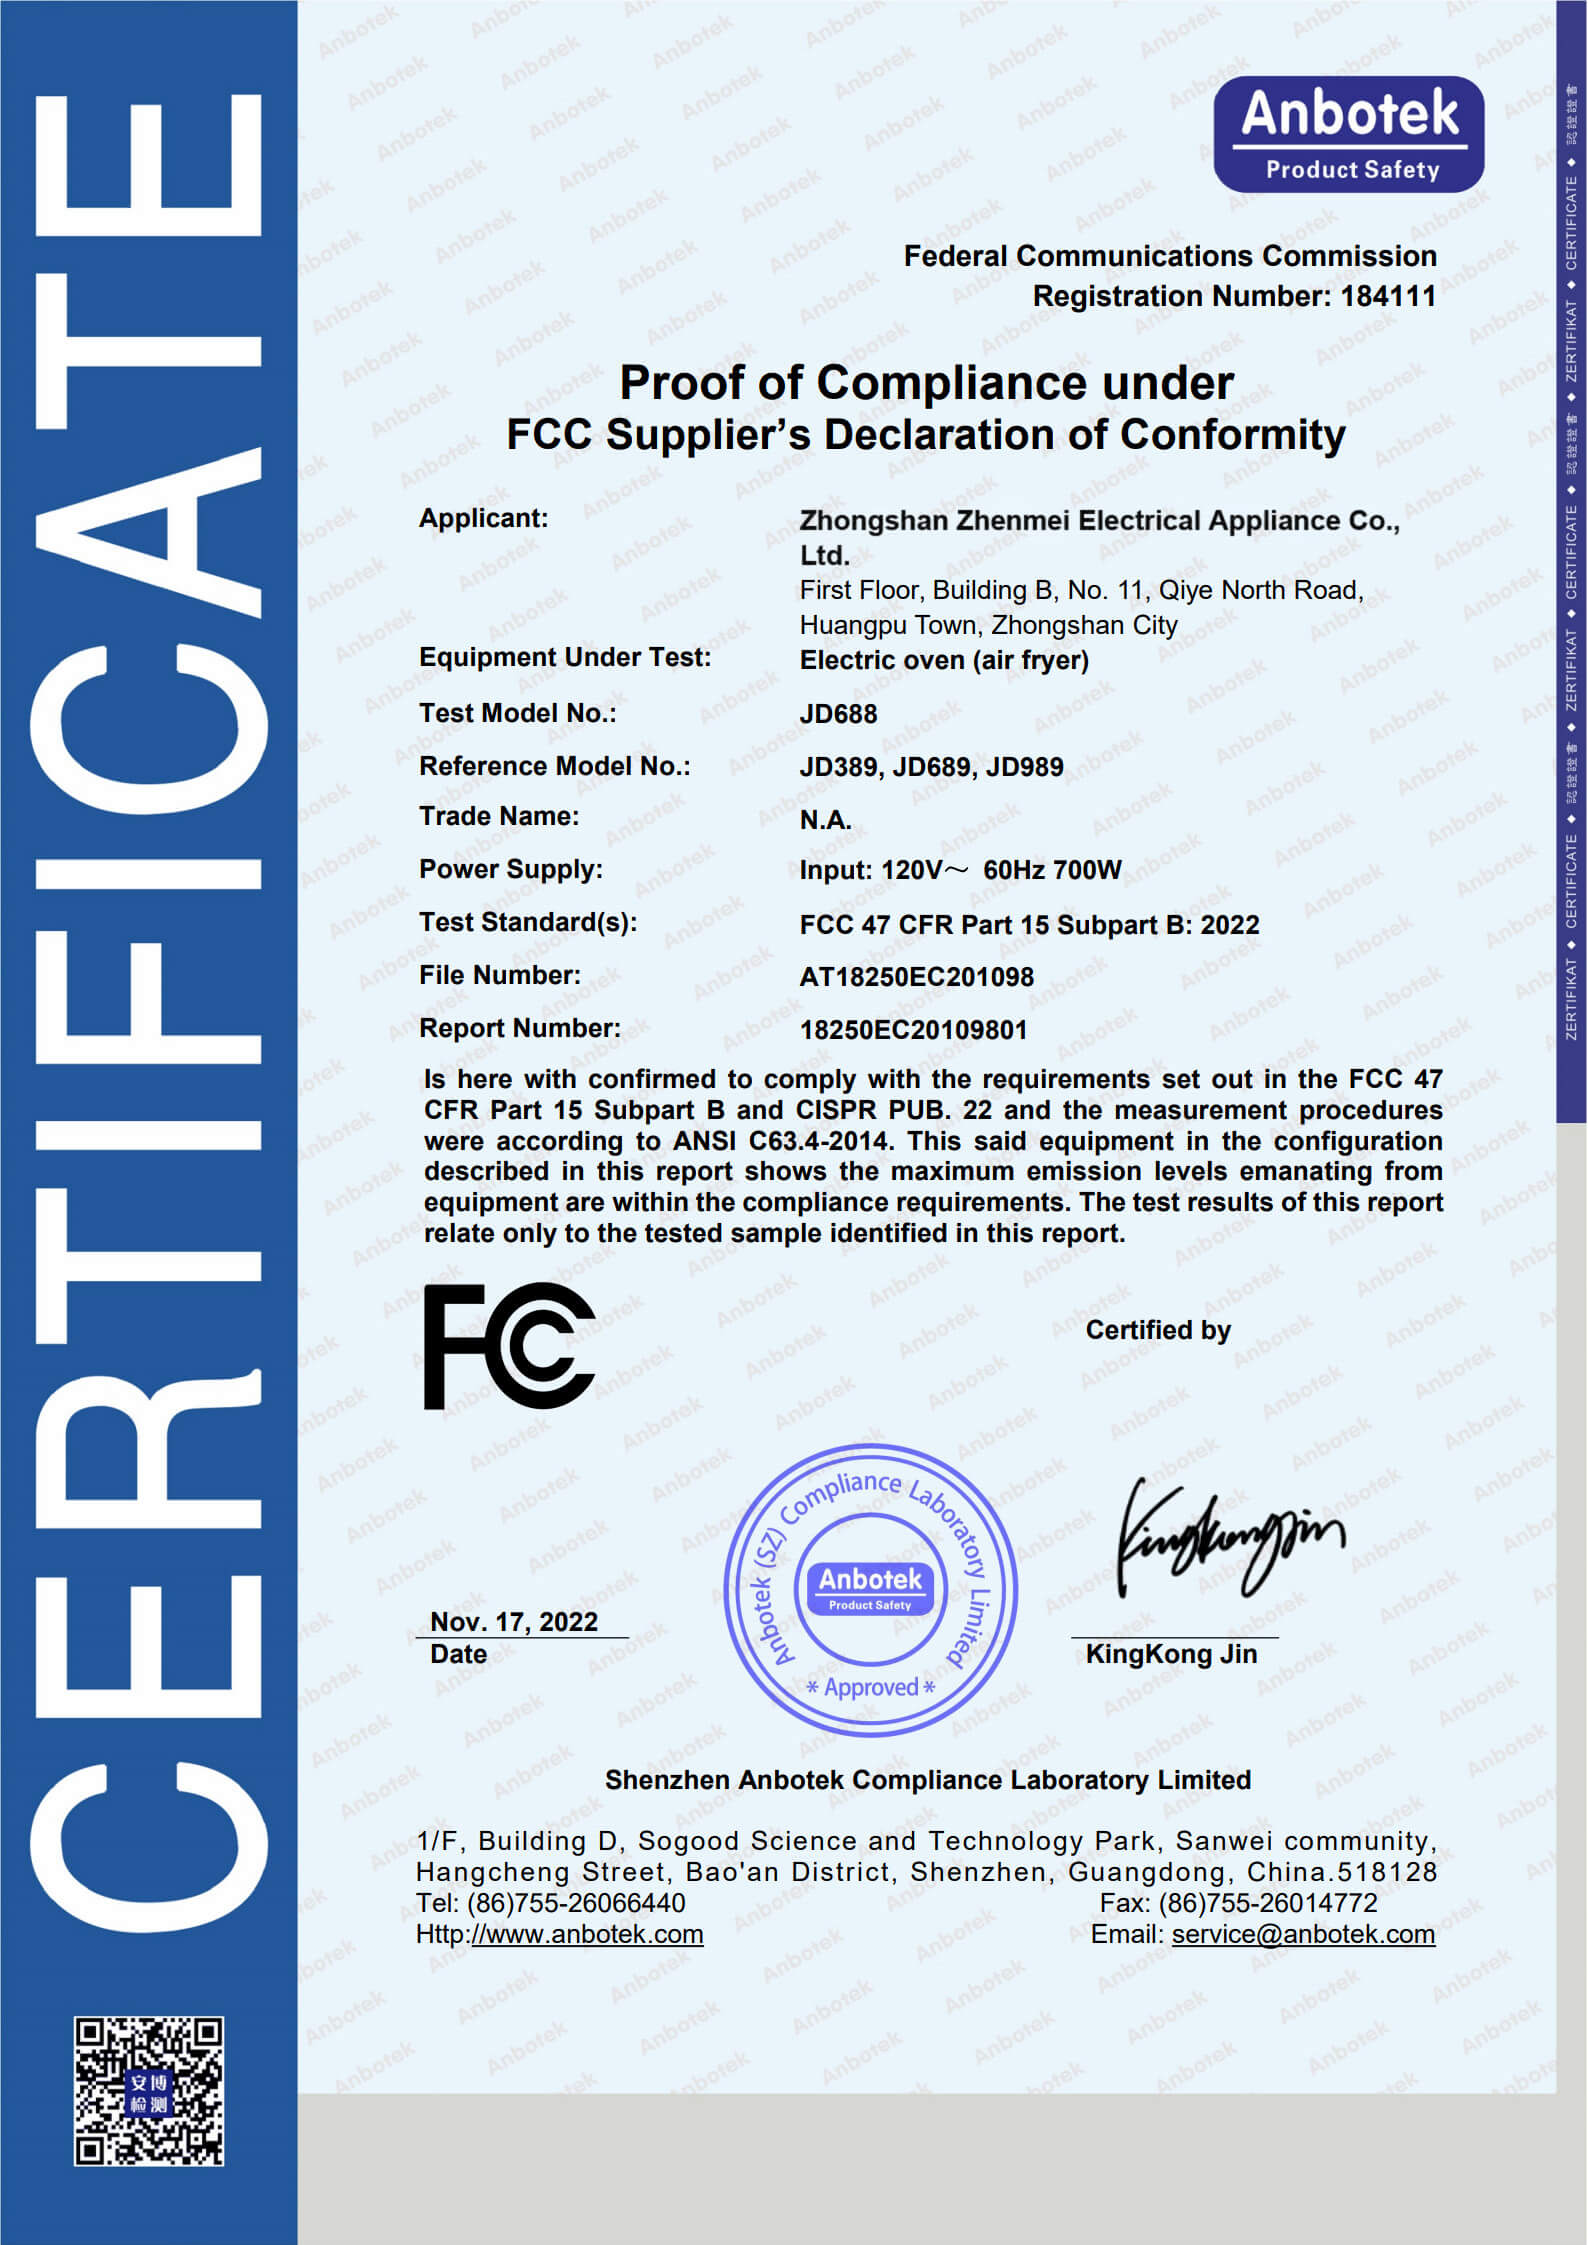
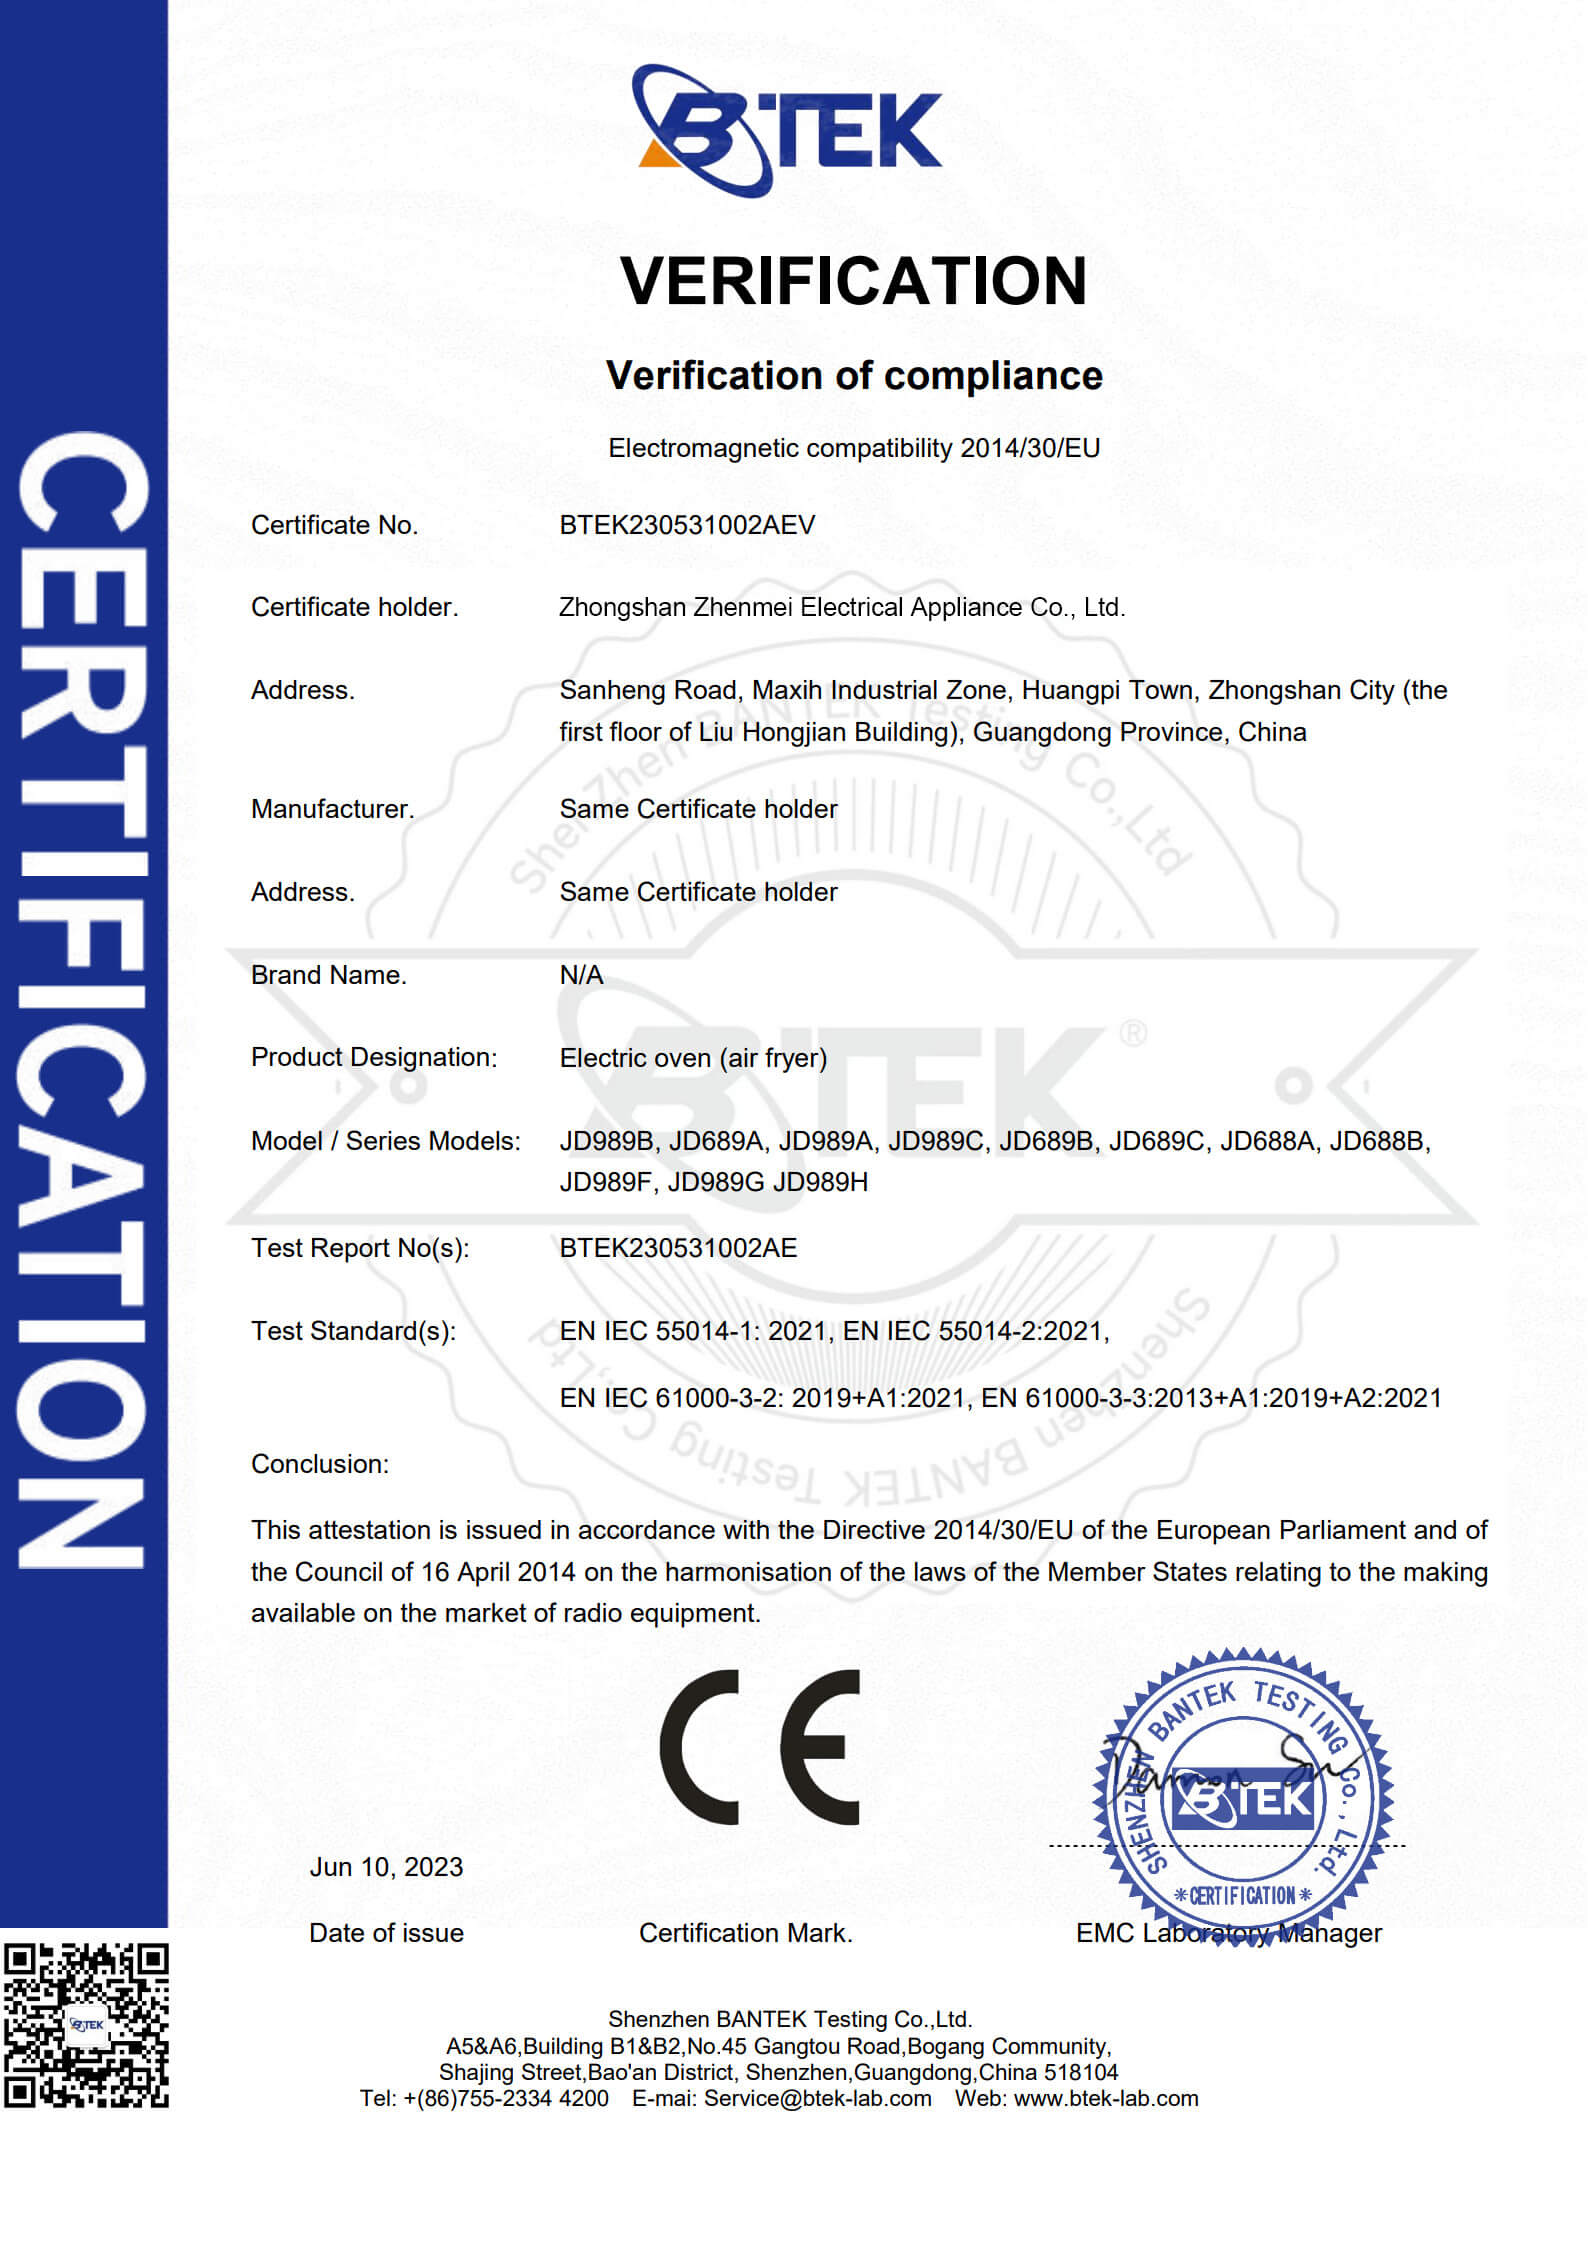
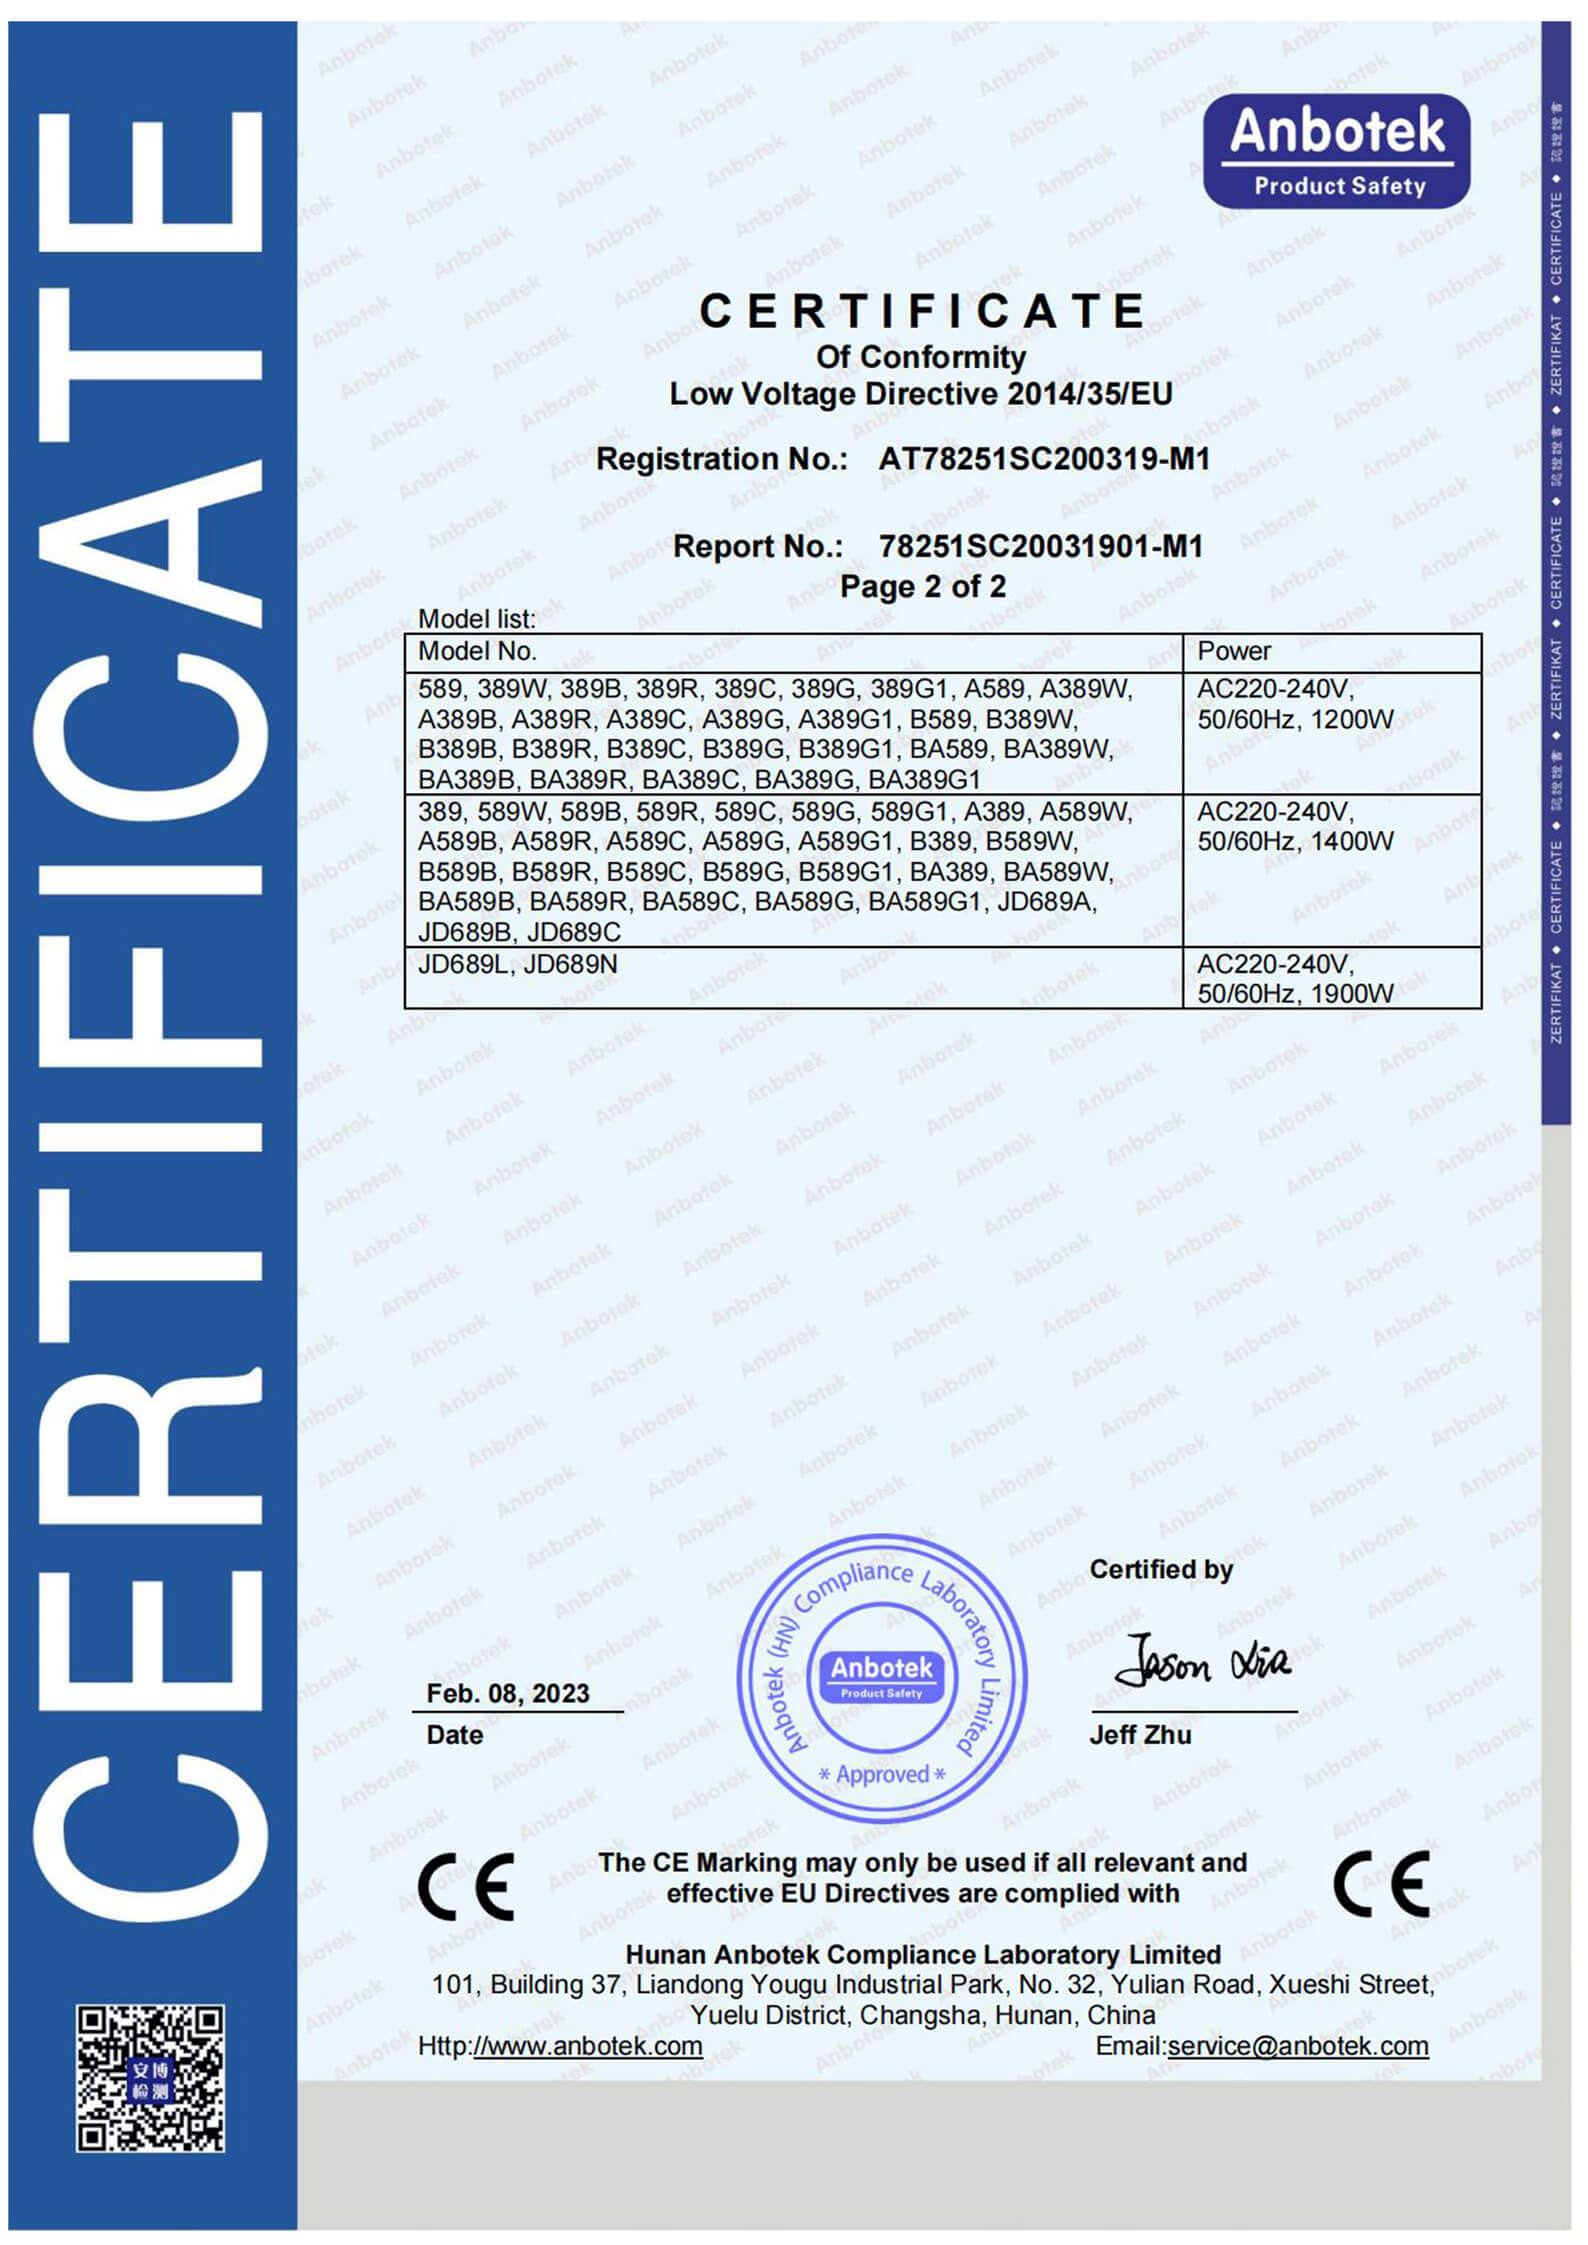
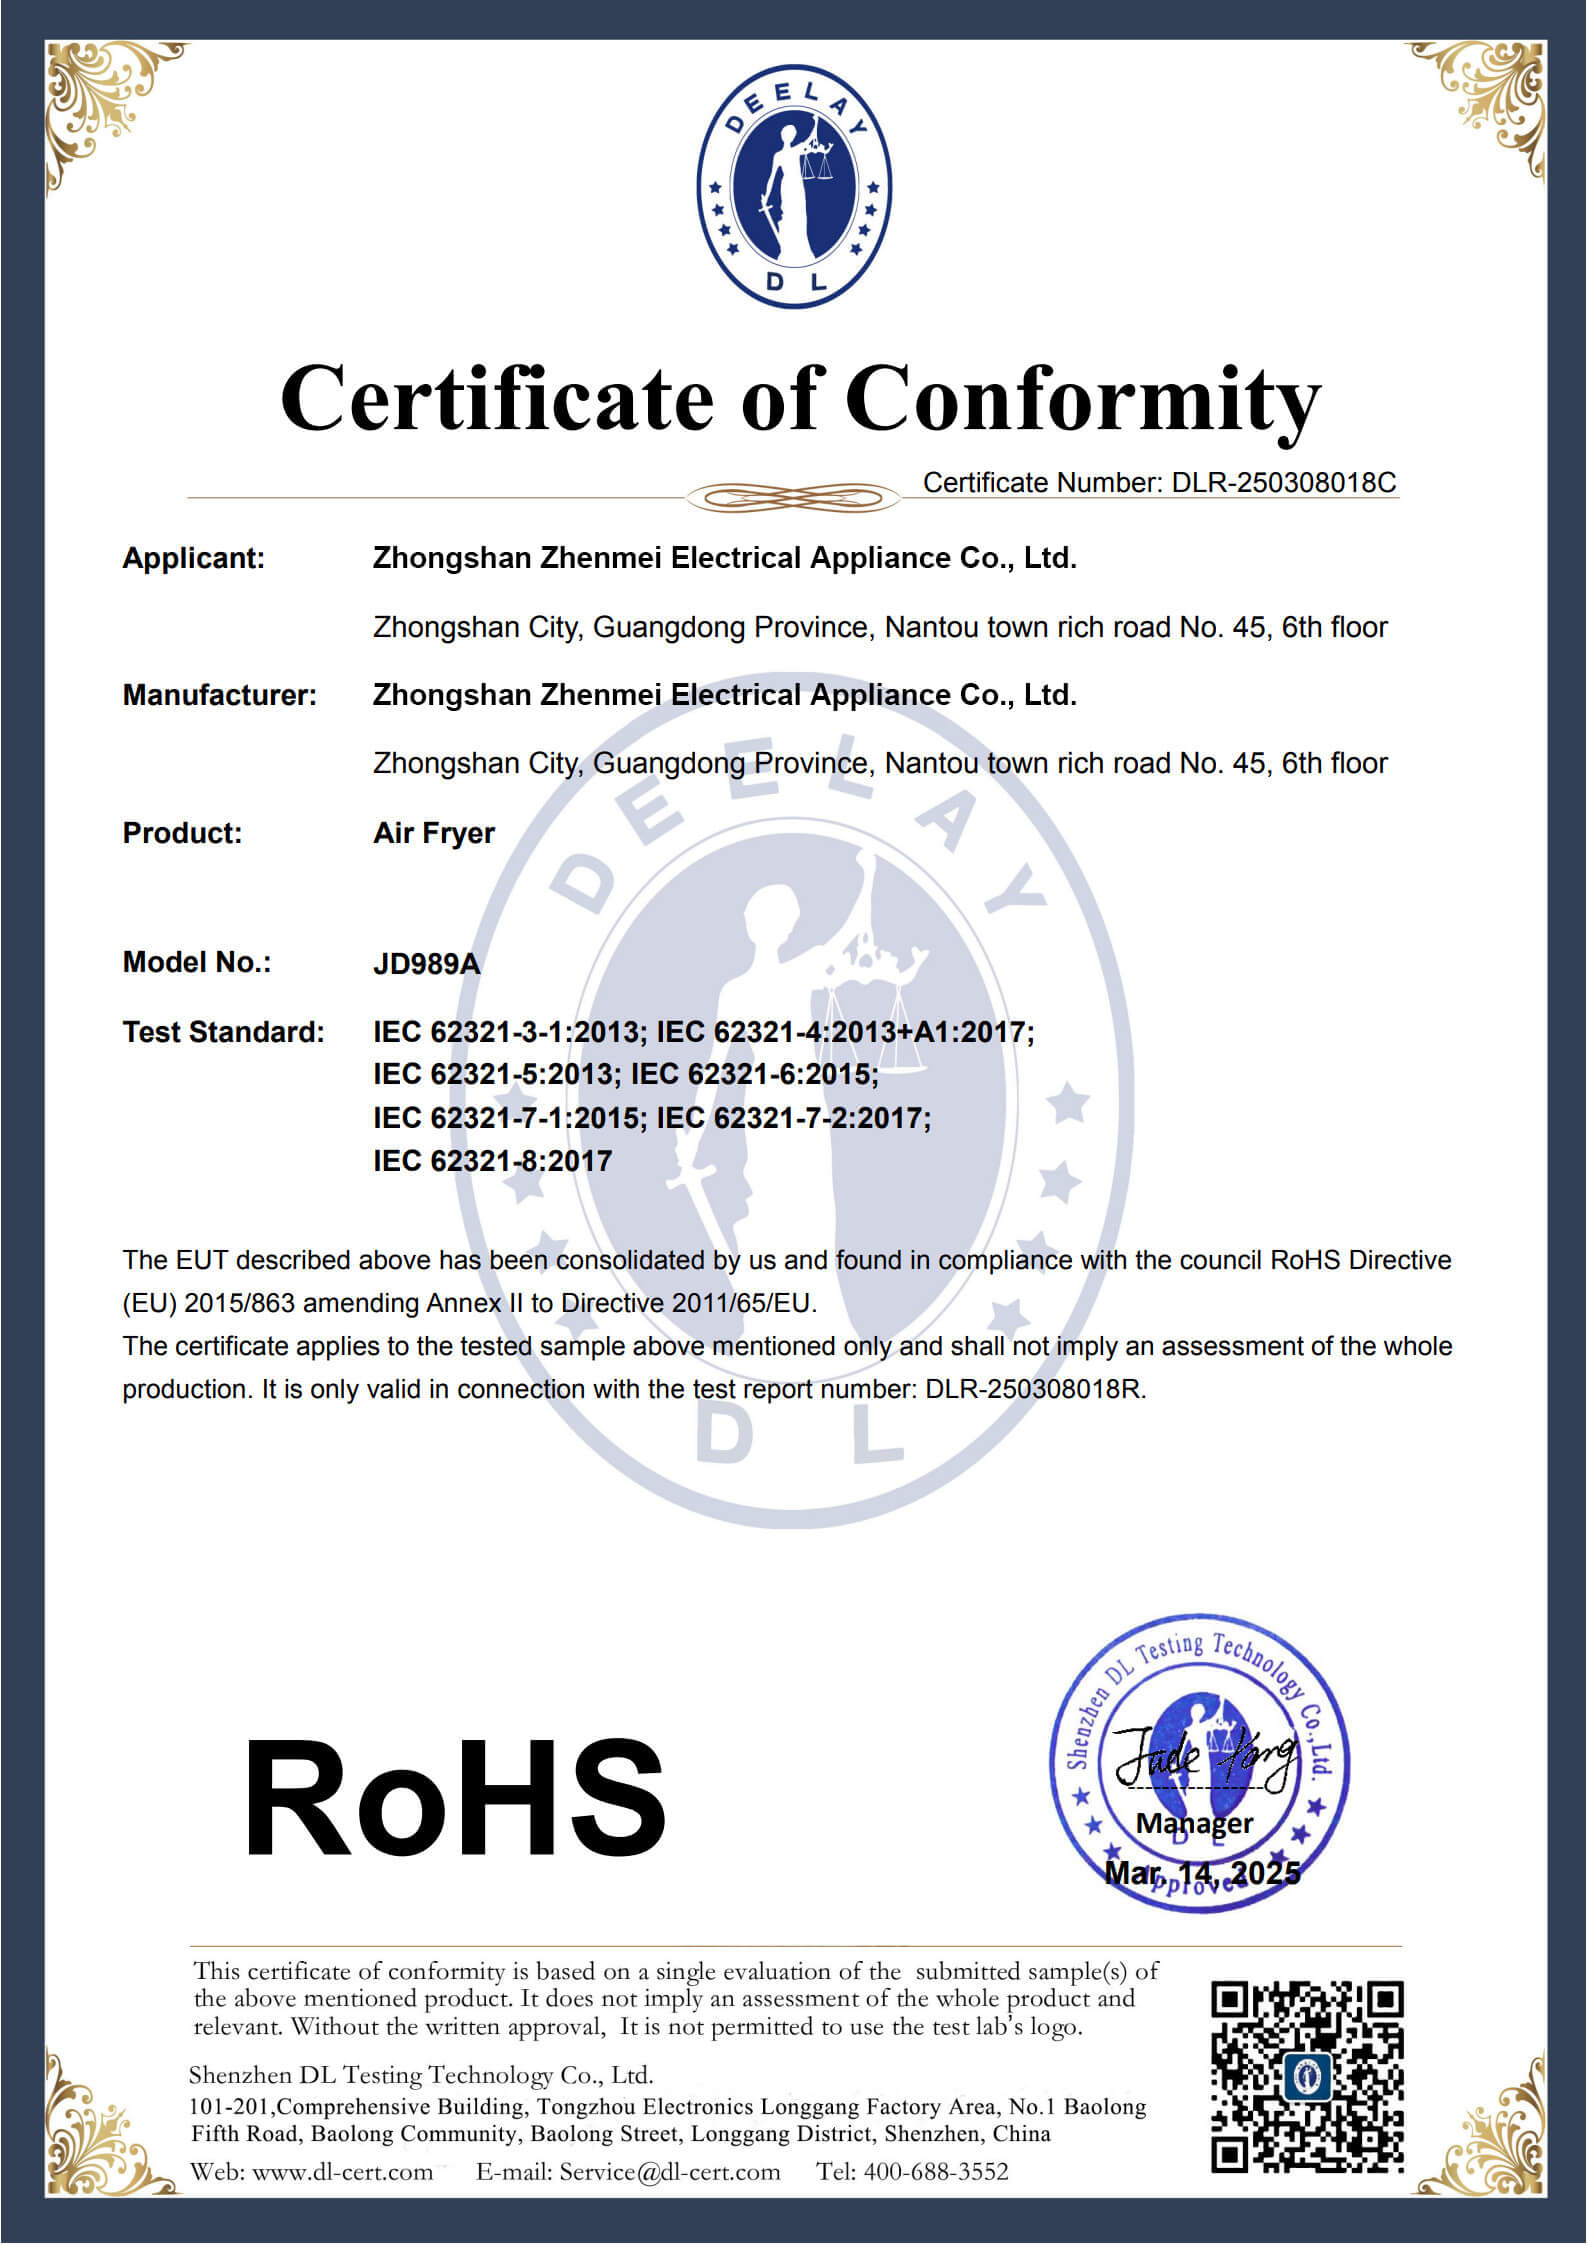
Founded with over 16 years of experience in kitchen appliance manufacturing, Zhongshan Zhenmei Electrical Appliance Co., Ltd. stands out as a premier OEM/ODM partner. Specializing in electric microwave ovens alongside air fryers, electric pressure cookers, and blenders, the company transforms innovative concepts into competitive, market-ready products.
Operating from a state-of-the-art 40,000 sqm manufacturing facility staffed by more than 300 professionals, including 20+ R&D experts, Zhenmei ensures rigorous quality control and high production volume—up to over 10,000 units daily. This scale and expertise support large restaurant chains, hospitality groups, and smart kitchen brands worldwide.
Zhenmei’s commitment to technology integration, sustainability, and customizable solutions makes it an ideal OEM collaborator to develop the next generation of electric microwave ovens tailored for restaurant pre-processing applications demanding reliability, precision, and energy efficiency.
All components and assembly operations are tightly controlled within a modern 40,000 sqm factory ensuring precision engineering and shorter time-to-market.
Daily output exceeding 10,000 units with robust quality management systems delivers reliable performance products for high-demand commercial environments.
Integrated design, manufacturing, and testing capabilities combined with flexible customization meet diverse brand requirements with scale efficiency.
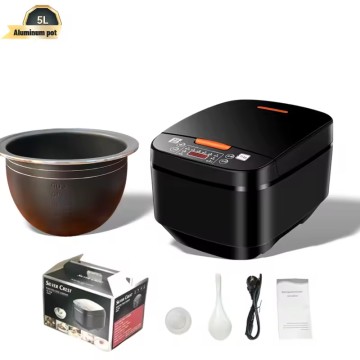 Aluminum Pot 5L Smart Digital Touch LCD Multi Non-Stick Silver Crest Home Electric Digital Rice Cooker
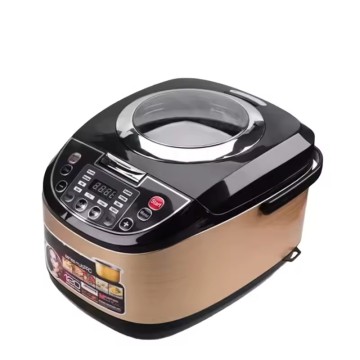 5L Smart Multi-Function Automatic Electric Digital Keep Warm Rice Cookers Smart Rice Cooker Silver Crest Rice Cooker
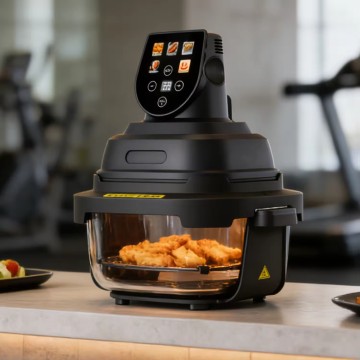 Glass Bowl Air Fryer With Visible Cooking Window Smart Digital Control Large Capacity Electric Air Fryer Oven Kitchen
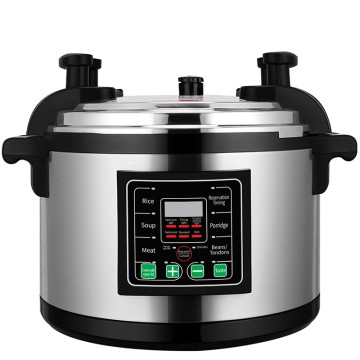 Commercial Electric Pressure Cooker 65L - 3500W Large Capacity
New Arrivals Large Capacity Deep Frying Pan Oven Visual Air Fryer
Air Fryer Oven Large Capacity 15L 10L 8L 6L 5L Digital Touch Smart Air Fryer With Glass Window for Home Kitchen
OEM Electric Oven for Baking Cake Bread Pizza Ovens 56L Kitchen Smart Home Toaster Oven
6L Smart Multi-function Automatic Electric Digital Keep Warm Crest Rice Cooker Support Customization