


AQL Sampling Explained for Kitchen Appliance Buyers
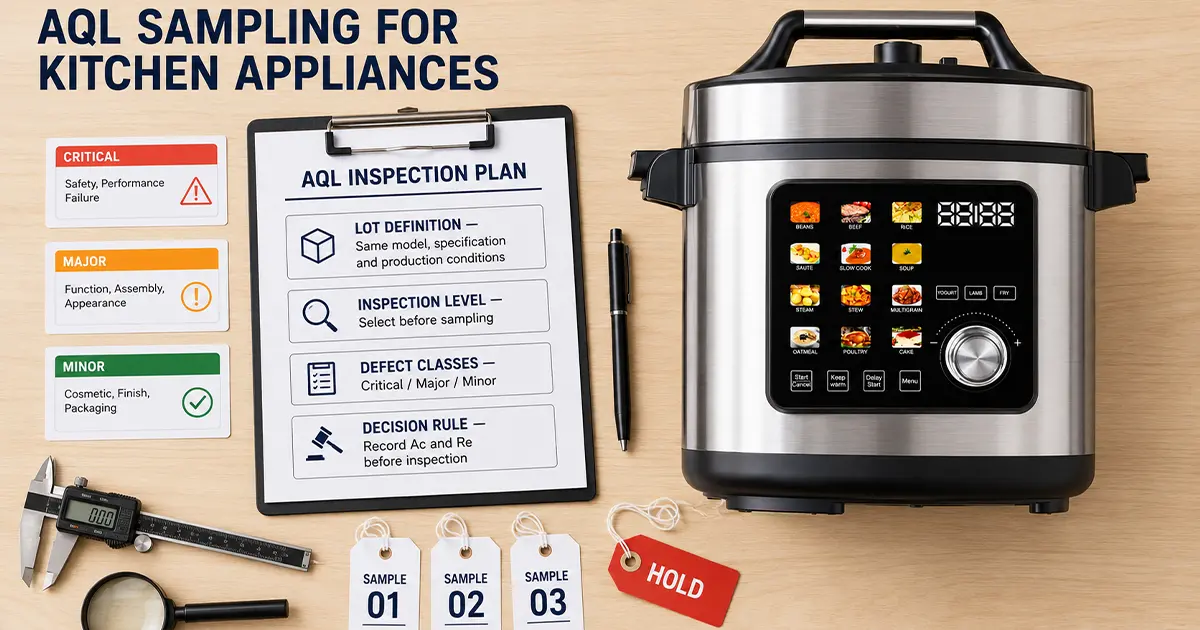
AQL sampling does not tell a buyer how many defects are acceptable in one shipment. It provides a structured way to select a sample and make a lot-acceptance decision. This guide explains how kitchen appliance buyers can define defect classes, choose an inspection level, read sample-size and Ac/Re tables, handle failed lots, and connect pre-shipment inspection with first-article approval, process controls and routine safety testing.
An approved sample does not guarantee that every unit in a finished production lot matches it. By the time a kitchen appliance order reaches pre-shipment inspection, the buyer must decide how many units to inspect, which defects matter most and what result will place the shipment on hold.
AQL sampling gives both buyer and supplier a common decision method. But it only works when the inspection plan is complete. Writing “AQL 2.5” in a purchase order is not enough: the lot, inspection level, sampling scheme, defect definitions and acceptance and rejection numbers must all be clear before inspection begins.
Key Takeaways
- AQL is an index used to select an acceptance-sampling plan; it is not a promise that a shipment contains exactly that percentage of defects.
- ISO 2859-1:2026 is now the current international edition for AQL-indexed lot-by-lot inspection and replaces the 1999 edition.
- General Inspection Level II with separate major and minor AQL values is a common starting point, not a universal kitchen-appliance requirement.
- Critical, major and minor defects must be defined with product-specific examples before the inspector starts.
- AQL lot acceptance cannot replace first-article approval, process control, routine safety tests, traceability or corrective action.
What AQL Means, and What It Does Not Mean
AQL stands for Acceptance Quality Limit. In an attribute-sampling plan, units or nonconformities are counted rather than measured as continuous data. The plan connects the lot size and inspection level to a sample-size code, then connects that sample size and the selected AQL to an acceptance number (Ac) and rejection number (Re).
The most important distinction is this: an AQL of 2.5 does not mean a buyer has agreed to accept 2.5% defective units in every shipment. It indexes a statistical sampling scheme designed for a continuing series of lots. A particular sample can contain fewer or more observed nonconformities, and the lot decision follows the Ac/Re rule in the selected table.
The current ISO edition is ISO 2859-1:2026, published in January 2026. It covers AQL-indexed single, double and multiple sampling schemes and includes normal, tightened, reduced and skip-lot concepts. Buyers using older quality agreements should check whether those documents still refer to the withdrawn 1999 edition. In the United States, ANSI/ASQ Z1.4:2003 (R2018) remains ASQ's current listed attribute-sampling edition as of this article's review date.
A Four-Step Method for Setting the Inspection Plan
| Step | Buyer decision | What must be documented |
|---|---|---|
| 1. Define the lot | Decide which finished units belong to one inspection lot. | SKU, version, quantity, production status, packing status and lot identity. |
| 2. Choose the level and scheme | Select normal, tightened or another authorized scheme and the inspection level. | Standard edition, single/double/multiple plan, inspection level and any switching rule. |
| 3. Classify defects | Agree what is critical, major or minor for this appliance and market. | Defect list with photographs, measurable criteria and severity rationale. |
| 4. Set the decision rule | Use the current licensed table to obtain sample size and Ac/Re values. | Code letter, sample size, AQL by defect class, Ac/Re and failed-lot action. |
General Inspection Level II is frequently chosen for normal final random inspections because it balances coverage and inspection effort. Level I may reduce the sample, while Level III generally increases it. Special levels S-1 to S-4 are intended for situations where smaller samples are necessary, often for costly, time-consuming or destructive checks. The right choice depends on risk and test burden, not on a rule that all appliances must use the same level.
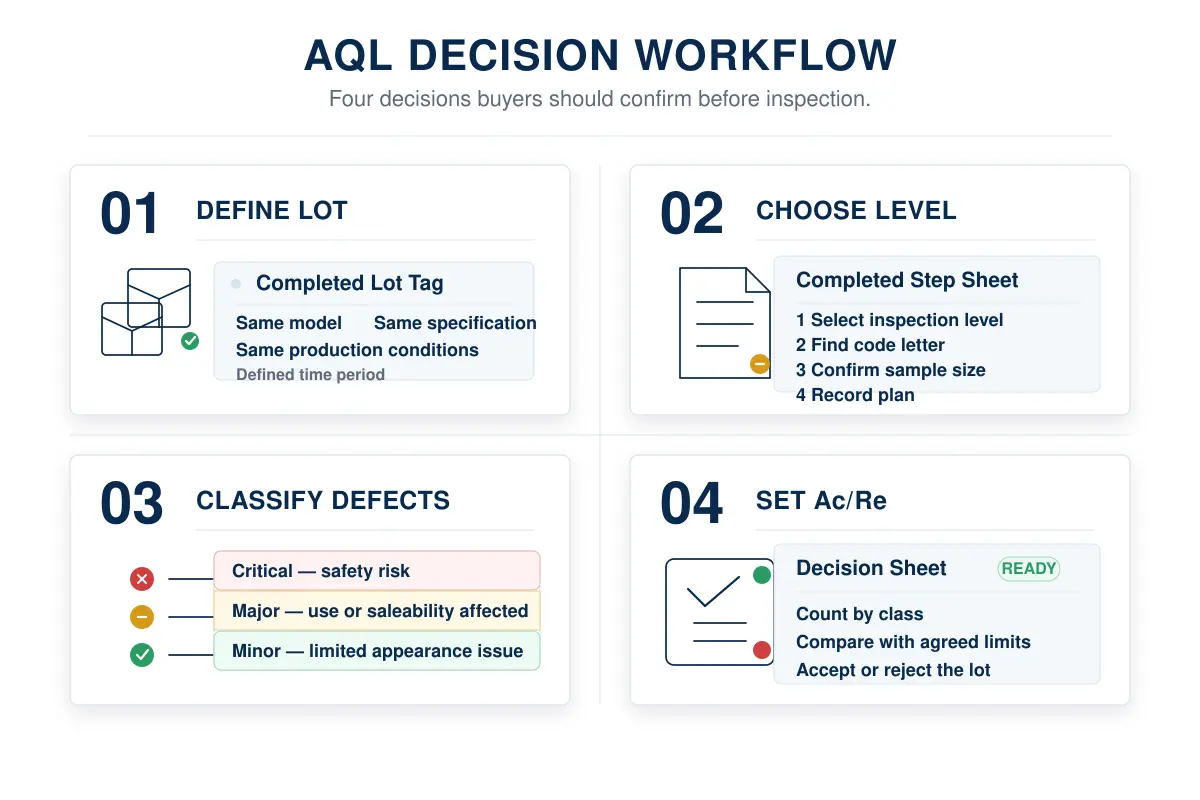
An AQL decision starts with a defined lot and defect standard, not with an isolated AQL number.
Classify Appliance Defects Before Selecting Numbers
The same physical issue can have different severity depending on product design, intended use and target market. A loose decorative trim may be minor on one model; a loose control component that exposes live parts may be critical. The defect catalogue must therefore be written for the actual appliance and approved sample.
| Class | Decision question | Kitchen appliance examples | Typical buyer treatment |
|---|---|---|---|
| Critical | Could the issue create an unreasonable safety or regulatory risk? | Accessible live part, failed protective earth connection, missing safety warning where required, serious overheating risk. | Buyers commonly specify a zero acceptance number or a separate stricter plan, plus immediate containment and investigation. |
| Major | Does the issue prevent intended use, materially reduce performance or create likely return risk? | Unit does not power on, temperature control fails, interlock does not operate, severe leakage, missing essential accessory. | A tighter AQL is commonly used than for cosmetic defects. |
| Minor | Does the issue affect appearance or workmanship without materially preventing normal use? | Small surface mark outside the primary viewing area, slight print misalignment or minor packaging finish issue. | A less stringent AQL may be agreed if the brand standard allows it. |
Many consumer-goods inspection plans start discussions around AQL 2.5 for major defects and 4.0 for minor defects. These values are commercial conventions, not ISO-mandated kitchen-appliance settings. Premium finishes, high return costs, new suppliers, complex heating systems or a history of failures may justify tighter requirements. The buyer should also define whether the plan counts defective units, individual nonconformities, or both.
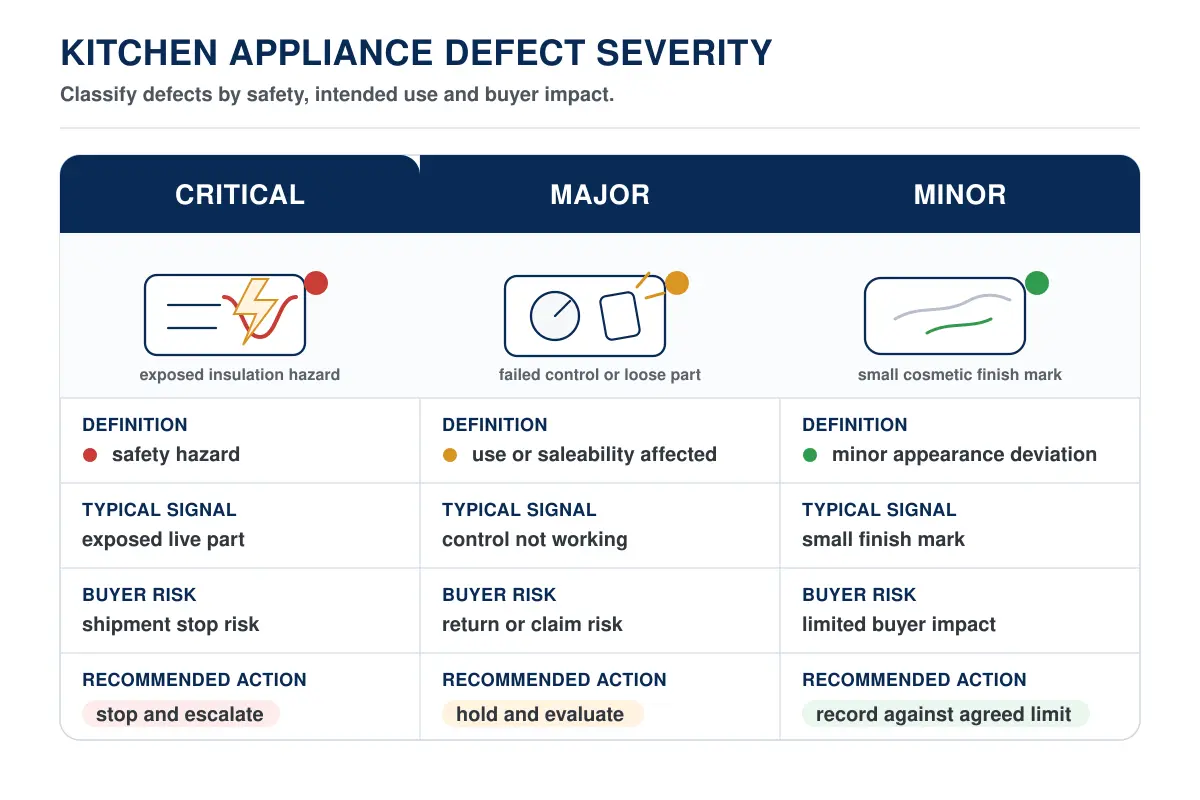
Defect severity should follow safety, intended use and customer impact rather than appearance alone.
How to Read the Sampling Tables
Do not calculate the sample size by applying the AQL percentage to the lot. The standard uses two linked lookups. First, the lot-size range and inspection level produce a sample-size code letter. Second, that code letter and selected sampling plan produce the sample size. The chosen AQL column then provides the Ac and Re values.
- Confirm the final lot quantity for one SKU and version.
- Use the lot-size and inspection-level table to find the code letter.
- Open the correct normal, tightened or reduced sampling table.
- Read the sample size and the Ac/Re pair for each defect class.
- Draw the sample randomly across cartons, pallet positions and production periods.
- Record every finding against the approved defect catalogue before making the lot decision.
Illustrative Scenario: A 500-Unit Appliance Lot
Assume a buyer has one finished lot of 500 identical appliances, chooses normal single sampling at General Inspection Level II, and uses the familiar table structure carried by common attribute-sampling systems. The lookup leads to code letter H and a sample of 50 units. Under a commonly used normal plan, AQL 2.5 for major defects corresponds to Ac 3 / Re 4, while AQL 4.0 for minor defects corresponds to Ac 5 / Re 6.
| Item | Illustrative setting | How to use it |
|---|---|---|
| Lot | 500 units, one SKU and version | Do not combine unrelated versions or reworked stock without agreement. |
| Inspection setup | Normal, single sampling, General Level II | Confirm the applicable standard edition and table before inspection. |
| Sample | Code H, 50 units | Select randomly across the completed lot. |
| Major decision | AQL 2.5, Ac 3 / Re 4 | Three major findings can accept on this criterion; four reject. |
| Minor decision | AQL 4.0, Ac 5 / Re 6 | Five minor findings can accept on this criterion; six reject. |
| Critical decision | Buyer-defined zero acceptance or separate plan | Stop and escalate any critical finding according to the quality agreement. |
Common AQL Mistakes and Their Consequences
| Common mistake | Likely consequence | Better practice |
|---|---|---|
| Writing only “AQL 2.5” | The inspector lacks a complete sample and decision plan. | Specify standard edition, scheme, level, defect classes and Ac/Re source. |
| Using one value for every defect | Cosmetic and safety issues receive the same treatment. | Separate critical, major and minor definitions and rules. |
| Letting the factory select convenient samples | The sample may not represent the lot. | Require random selection across cartons and production periods. |
| Counting only defective units without recording defects | Repeated failure modes and root causes remain hidden. | Record both unit disposition and each observed nonconformity. |
| Automatically releasing after rework | Unverified rework can introduce new defects. | Define containment, reinspection and release authority in advance. |
| Using an obsolete standard reference | Buyer, supplier and inspector may consult different tables or rules. | State the edition and update agreements referring to withdrawn versions. |
When AQL Sampling Is Not Enough
AQL final inspection is one gate in a larger quality system. It cannot confirm that an unapproved component was not substituted earlier in production. That requires version control and component traceability. It also cannot prove that the mass-production process matches the approved design unless the project has a controlled first article inspection and clear change-management rules.
For electrical, thermal and protective functions, buyers should confirm which checks the factory performs as routine production tests, at what frequency and against which product-specific requirements. A final random sample does not replace defined line controls or the documented production process. Destructive tests, endurance tests and measurements that consume substantial time may use separate special levels or test plans.
Supplier capability matters as much as the final count. A structured factory audit checklist can reveal whether calibration, nonconforming-product control, training and corrective-action systems exist before the first lot is produced. This is often more valuable than simply tightening AQL after recurring failures.
Honest Advice
Do not choose the tightest possible AQL merely to appear quality-focused. An unrealistically strict plan can create repeated disputes without improving the process. Define defects around actual user, safety and return risk; match inspection effort to that risk; and invest in prevention where the cost of poor quality is highest.
What to Do When the Lot Fails
A failed AQL result should place the lot on hold. It should not automatically trigger shipment cancellation, price negotiation or informal approval. The quality agreement should identify who can release the lot and what evidence is required.
- Contain: identify the affected lot, versions, cartons and related production periods.
- Confirm: review defect classification, photographs, test method and count accuracy.
- Investigate: determine whether the issue is isolated, systematic or linked to a component or process change.
- Correct: define rework, sorting, replacement or reproduction with clear responsibility.
- Reinspect: use the agreed reinspection or tightened plan; do not reuse convenient units from the first sample.
- Release: obtain documented buyer approval before shipment and retain the inspection and corrective-action records.
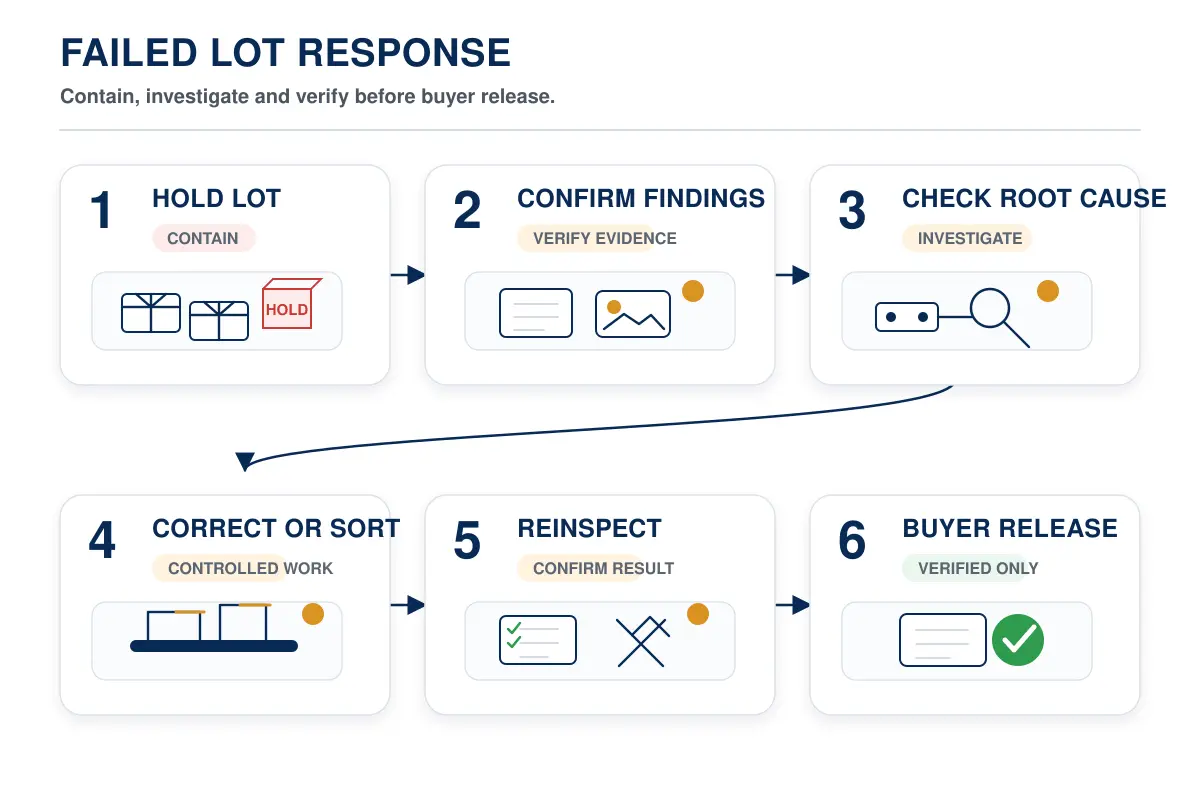
A failed lot needs containment, root-cause review and verified reinspection before release.
AQL Checklist for the Purchase or Quality Agreement
- Current sampling standard and edition are named.
- Lot definition identifies SKU, version, quantity and production status.
- Inspection scheme and level are specified.
- Normal, tightened, reduced and reinspection conditions are defined where applicable.
- Critical, major and minor defects include product-specific examples.
- AQL and Ac/Re source are stated for each defect class.
- Random sample selection method covers cartons and production periods.
- Functional, visual, packaging and safety-related checks are listed.
- Failed-lot containment, rework and reinspection responsibilities are agreed.
- Buyer release authority and required records are documented.
These requirements should also align with the broader OEM and ODM project scope. Product configuration, packaging, plug, control panel and component changes can all affect the defect catalogue and the lot identity used for inspection.
Limitations Buyers Should State Clearly
AQL sampling makes a probability-based lot decision; it does not guarantee that every shipped unit conforms. Results depend on random selection, inspector consistency, accurate defect definitions and correct use of the applicable table. A plan designed for continuing lots may also be inappropriate for an isolated purchase without adjustment.
This article reflects ISO and ASQ information checked on July 30, 2026. Buyers should obtain the licensed standard or work with a qualified quality professional before placing Ac/Re values into a binding agreement. Product safety, conformity assessment and routine test requirements remain product- and market-specific.
Conclusion
AQL works best as a shared decision system, not as a number added to the bottom of an inspection request. Define the lot, choose the scheme and level, classify defects, read the correct current table and agree what happens after a failure. For many consumer-appliance orders, GII with separate major and minor values can be a practical starting point, but the final settings should follow product risk, supplier history, brand expectations and test cost.
The strongest quality plans connect final sampling with approved samples, component versions, process controls, routine safety checks and corrective action. That combination helps buyers prevent recurrence rather than repeatedly sorting defects at the shipping gate.
FAQ
Does AQL 2.5 mean that 2.5% defective products are acceptable?
No. AQL 2.5 indexes a sampling scheme used to make lot decisions over a continuing series of lots. The inspector uses the selected table's sample size and Ac/Re numbers; the observed defect percentage in one sample is not itself the AQL definition.
Is General Inspection Level II mandatory for kitchen appliances?
No. GII is a common normal-inspection starting point. Buyers may choose another general or special level based on product risk, supplier performance, test cost and the purpose of the inspection.
Should critical defects use AQL 0 or 0.65?
There is no single universal answer for every appliance and agreement. Many buyers specify a zero acceptance number for defined critical defects or use a separate stricter plan. The contract should state the exact rule rather than relying on an ambiguous label.
What changed in ISO 2859-1:2026?
The third edition replaced ISO 2859-1:1999 and its amendments. ISO's published overview highlights integrated skip-lot sampling procedures and updated guidance for applying sampling strategies, alongside AQL-indexed single, double and multiple schemes.
What happens after an AQL failure?
The lot should remain on hold while the parties confirm findings, contain affected stock, investigate root cause and agree correction. Reinspection should follow the contract's defined plan, and shipment should require documented release.
Can AQL replace 100% production-line safety testing?
No. Final random sampling and routine production tests serve different purposes. Buyers should define which safety-related checks are performed on every unit or at another required frequency and which checks belong to the final random inspection.
Plan the Inspection Before Production Starts
If you are preparing a kitchen appliance order, share the product category, order quantity, target market, approved sample status, defect categories and intended inspection stage through the APEXDURA contact form. The project team can review how those requirements fit into the sourcing and production workflow before the lot reaches final inspection.