


Inside APEXDURA’s Metal Stamping Workshop
Metal stamping is one of the practical foundations behind many kitchen appliance parts. From sheet material and forming dies to appliance baskets, bowls, brackets and structural metal parts, the stamping workshop helps turn flat metal into repeatable components ready for assembly. This photo-based article takes buyers inside APEXDURA’s metal stamping area and explains why it matters for OEM/ODM appliance projects.
When buyers inspect a finished kitchen appliance, they usually notice the final shape, fit, surface, handle feel and packaging. Behind those visible details, however, many metal parts have already passed through material preparation, stamping, forming, trimming, handling and inspection before they ever reach assembly.
APEXDURA’s metal stamping workshop supports that upstream manufacturing work. The photos in this article show stamping presses, sheet metal coils, round blanks, formed appliance baskets and semi-finished metal parts inside the workshop. Rather than treating these photos as decoration, this article explains what buyers should understand from them: metal part control is closely tied to product structure, appearance, assembly fit and batch consistency.
Key Takeaways
- Metal stamping helps form key appliance components such as baskets, bowls, shells, supports and other structural metal parts depending on the product design.
- For OEM/ODM buyers, the stamping workshop matters because metal part variation can affect assembly fit, appearance, coating, packaging and finished product quality.
- Good stamping control is not only about pressing metal into shape; material handling, tooling setup, first-piece review, edge quality and semi-finished part protection also matter.
- The workshop photos show real production context, but this article avoids unconfirmed claims about machine count, tonnage, daily output or defect rate.
- Buyers should connect metal stamping review with sample approval, first article inspection, production process control and final shipment checks.
Why Metal Stamping Matters in Kitchen Appliances
Kitchen appliances often combine plastic, metal, electrical and packaging parts into one finished product. Metal parts are not always the most visible element, but they can strongly influence how a product feels and performs in daily use. A basket needs stable shape. A bowl or inner liner needs consistent forming. A bracket or support part needs to align with assembly. A shell or panel needs to fit the design without creating gaps or deformation.
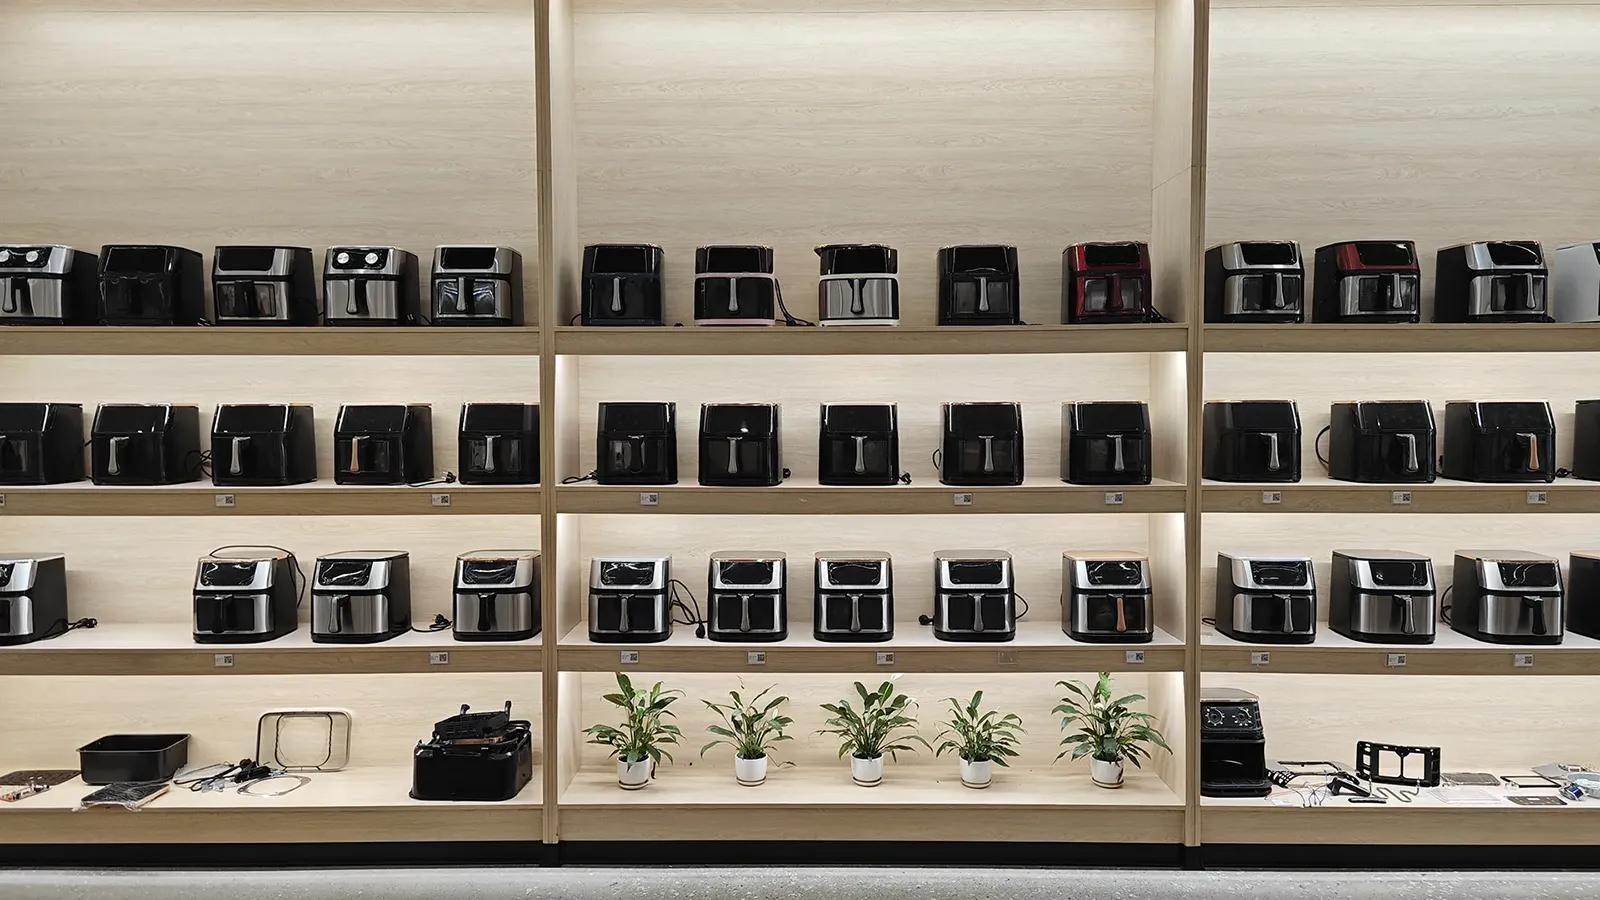
For APEXDURA’s current product lines, metal parts may support categories such as air fryers, ovens, electric pressure cookers, microwaves, meat grinders, blenders, juicers and coffee machines, depending on each model’s structure and specification. The exact part scope is model-specific, but the sourcing question is always similar: can the supplier make repeatable metal parts that support the finished appliance?
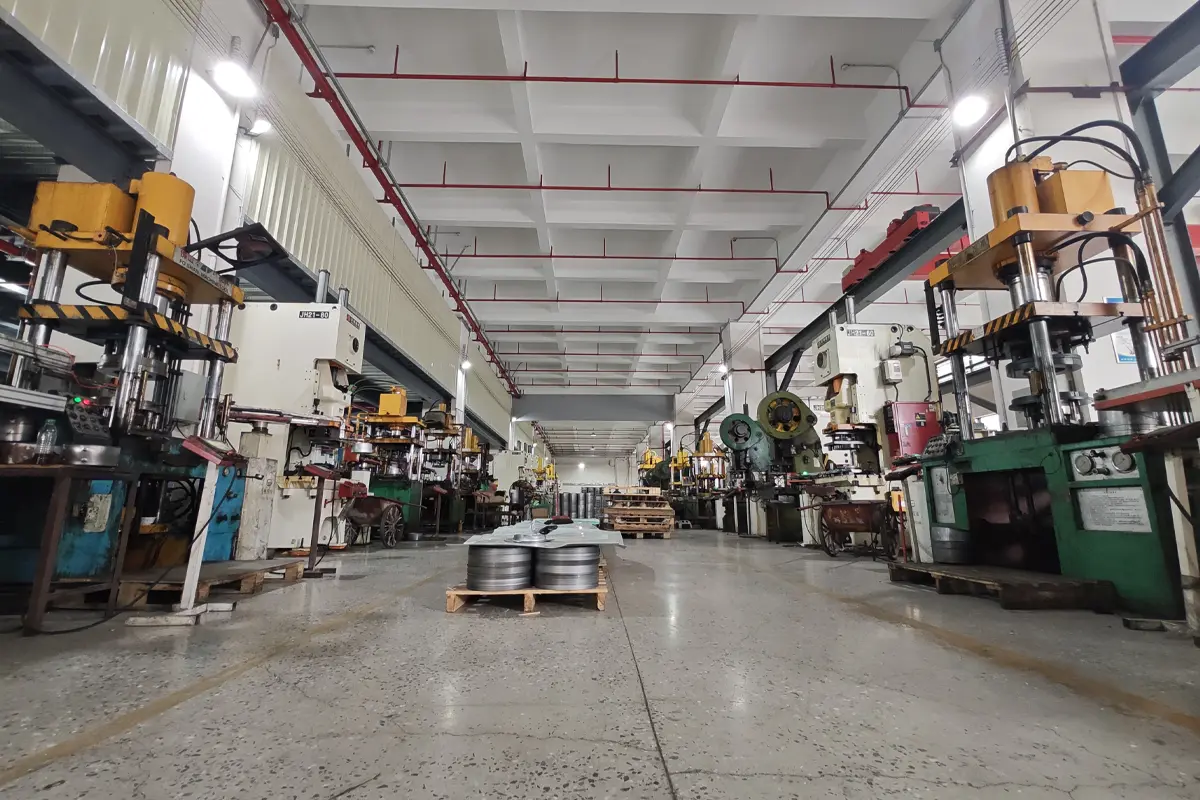
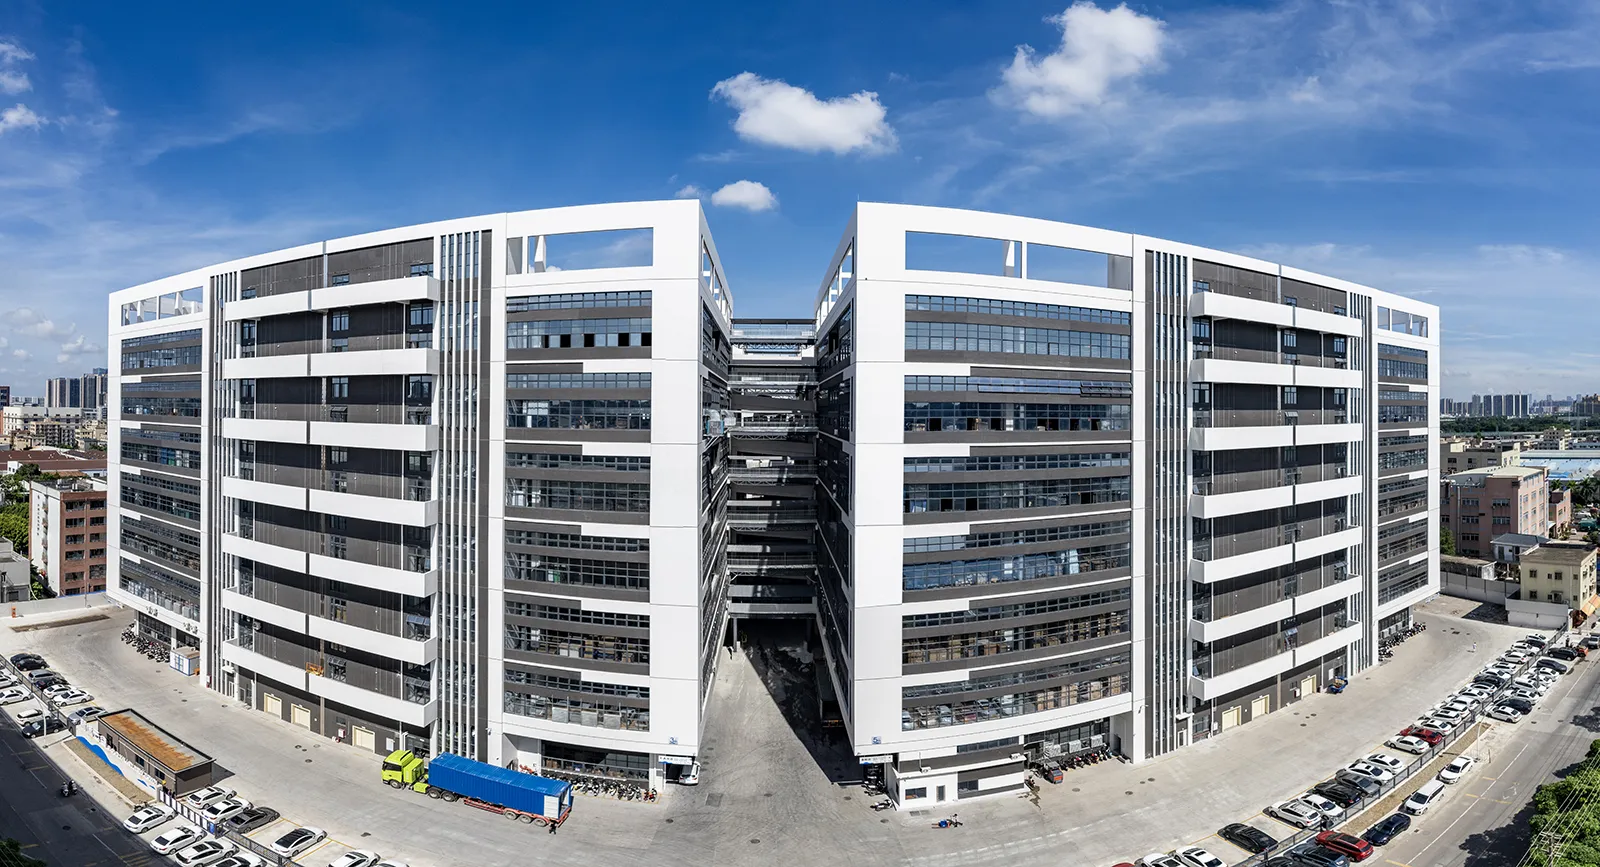
A wide workshop view shows metal stamping as an upstream production area, not just a single machine operation.
From Sheet Material to Formed Components
Metal stamping starts with material control. The workshop photos show sheet coils, round blanks and stacked metal pieces waiting for the next process. These are not finished products yet. They are part of the controlled route from raw sheet material to formed appliance components.
For buyers, this stage matters because material condition affects later forming and assembly. Thickness, surface condition, handling marks, storage method and batch separation can all influence production stability. A metal part that looks simple in the final product may require several upstream decisions before it can be formed consistently.
| Workshop stage | What buyers can see | Why it matters |
|---|---|---|
| Sheet or coil preparation | Metal coils, sheets or cut blanks arranged near the line. | Material condition influences forming stability and surface quality. |
| Blanking or pre-cutting | Round or shaped blanks prepared before forming. | Consistent blank size helps reduce forming variation. |
| Stamping and drawing | Presses and dies shape metal into baskets, bowls or structural parts. | Tooling setup affects dimensions, edge quality and repeatability. |
| Trimming and hole forming | Edges, openings, fixing points or ventilation features may be added. | Small metal details can affect assembly and user safety. |
| Part transfer and storage | Finished or semi-finished metal parts stacked and protected for next process. | Good handling reduces deformation, scratches and mixed batches. |
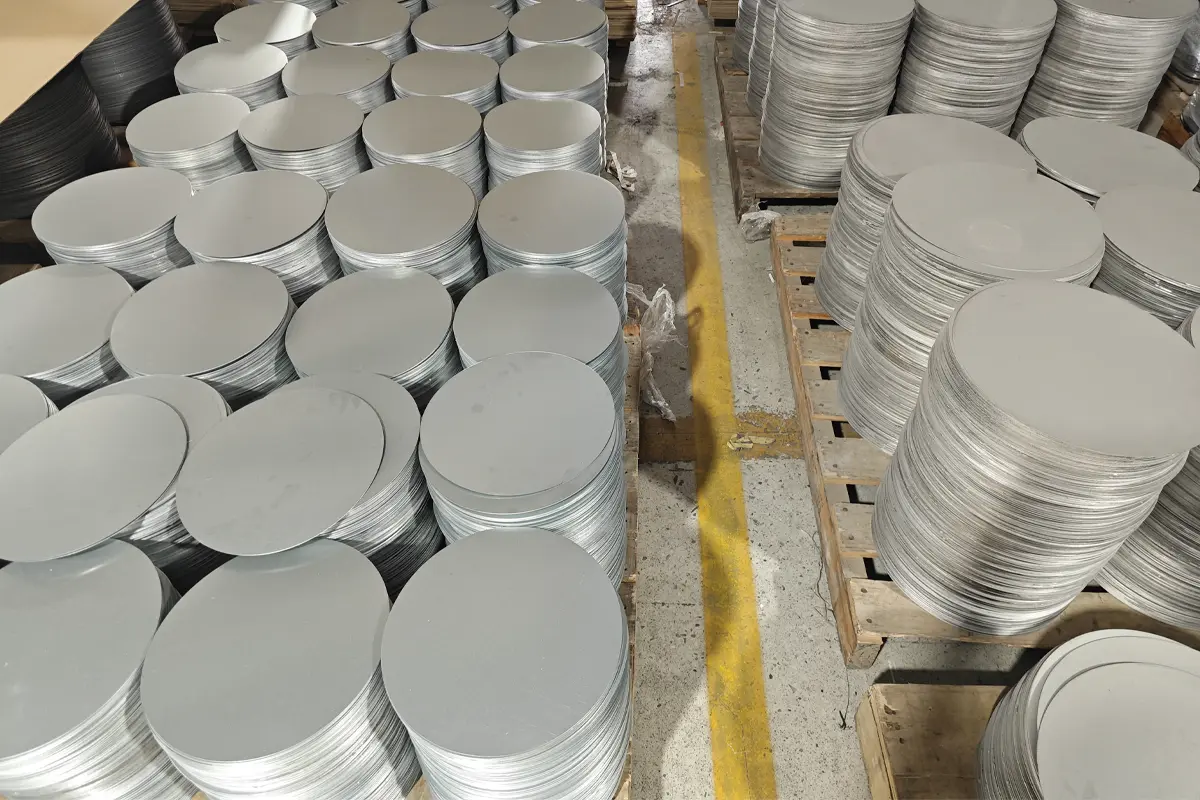
Prepared metal blanks show the step between sheet material and formed appliance components.
Stamping Presses and Tooling Setup
The workshop includes multiple stamping and forming machines. Their role is to apply force through tooling so that flat metal can be cut, bent, drawn or formed into the required part geometry. The exact process depends on the component: a shallow tray, a deeper basket, a circular part and a structural support may require different tools and control points.
For a buyer, the important question is not the appearance of the machine alone. It is whether the stamping process is linked to the approved part, the correct tooling, the required edge condition and the final assembly need. Tooling setup, first-piece confirmation and part handling can all affect whether a batch remains consistent.
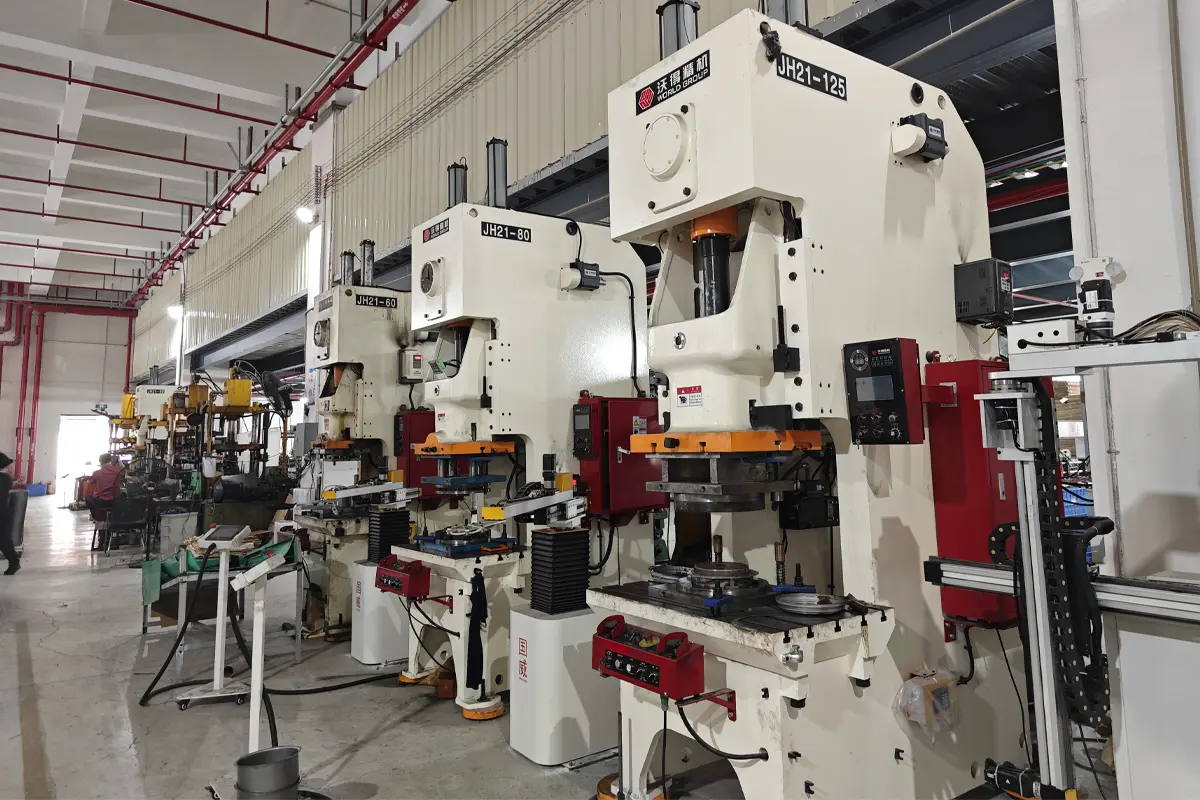
Stamping presses and tooling stations form metal parts before they move toward assembly or surface treatment.
What We Watch During Metal Part Production
A stamped metal part can create problems if the edge is sharp, the shape is unstable, the holes do not align, the depth varies, the surface is scratched or the part deforms during handling. These issues may look small at the component level but become much more expensive after assembly or shipment.
That is why metal part review should include more than one visual check. The team needs to consider material condition, tooling setup, first-piece confirmation, dimensional consistency, edge condition, surface marks and batch handling. For coated or painted parts, the downstream finishing process also needs to be considered.
| Check area | Examples | Possible impact if missed |
|---|---|---|
| Shape and depth | Basket shape, bowl depth, panel curvature or formed corner stability. | Poor assembly fit or visible product inconsistency. |
| Edge condition | Burrs, sharp edges, trimming marks or deformation. | User handling risk, coating difficulty or rework. |
| Hole and fixing alignment | Rivet holes, screw positions, ventilation slots or mounting points. | Assembly delay, loose parts or mismatch with other components. |
| Surface condition | Scratches, dents, oil marks or uneven surface before coating. | Appearance issues after finishing or customer complaints. |
| Batch separation | Clear separation of models, versions or production lots. | Mixed parts, wrong assembly and traceability problems. |
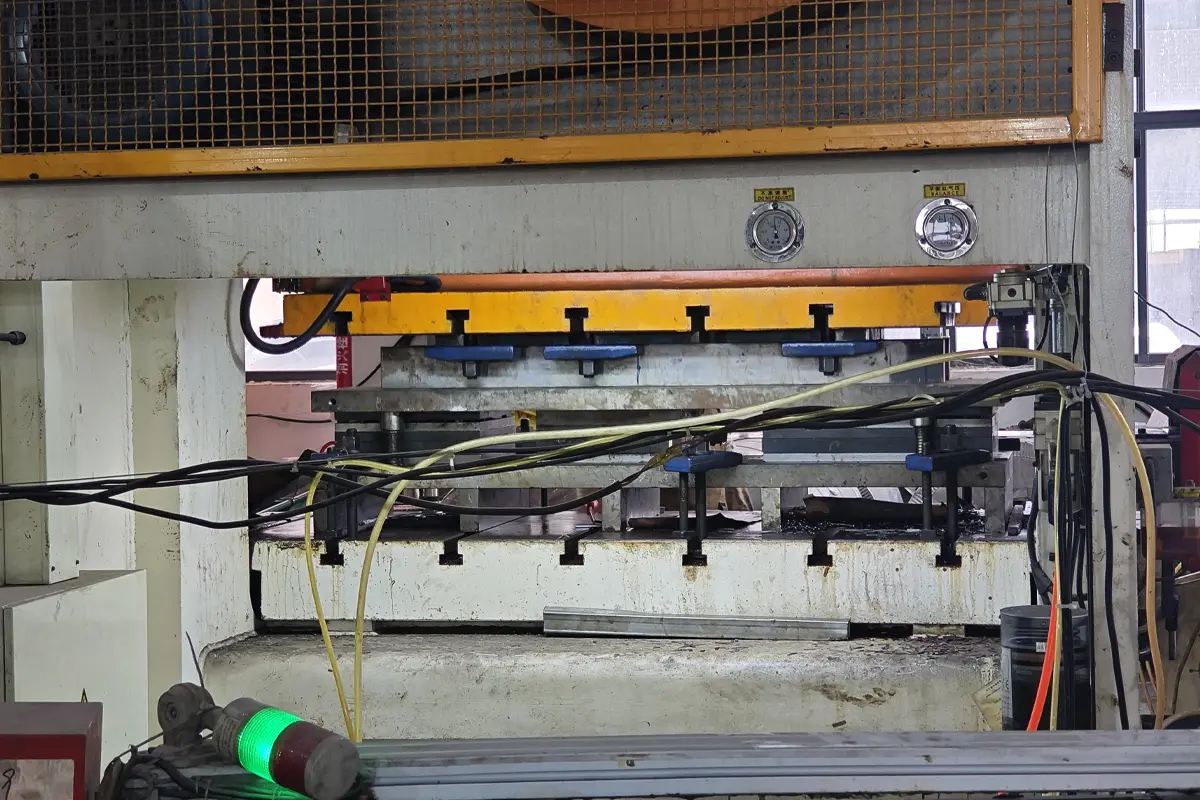
Tooling setup and first-piece review help keep metal parts aligned with the approved product requirement.
From Stamped Parts to Appliance Assembly
Once metal parts are formed, they still need to be handled carefully. The photos show stacks of formed metal baskets and semi-finished parts protected with film and moved through the workshop. This stage is easy to underestimate. A part can be correctly stamped but later scratched, dented, mixed or deformed if transfer and storage are not controlled.
For appliance buyers, this is where metal stamping connects directly with final production. A basket or bowl must fit the product design. A housing or bracket must match assembly fixtures. A visible metal component should be protected before coating, packing or assembly. The better the semi-finished part control, the less pressure is placed on final inspection to catch preventable problems.
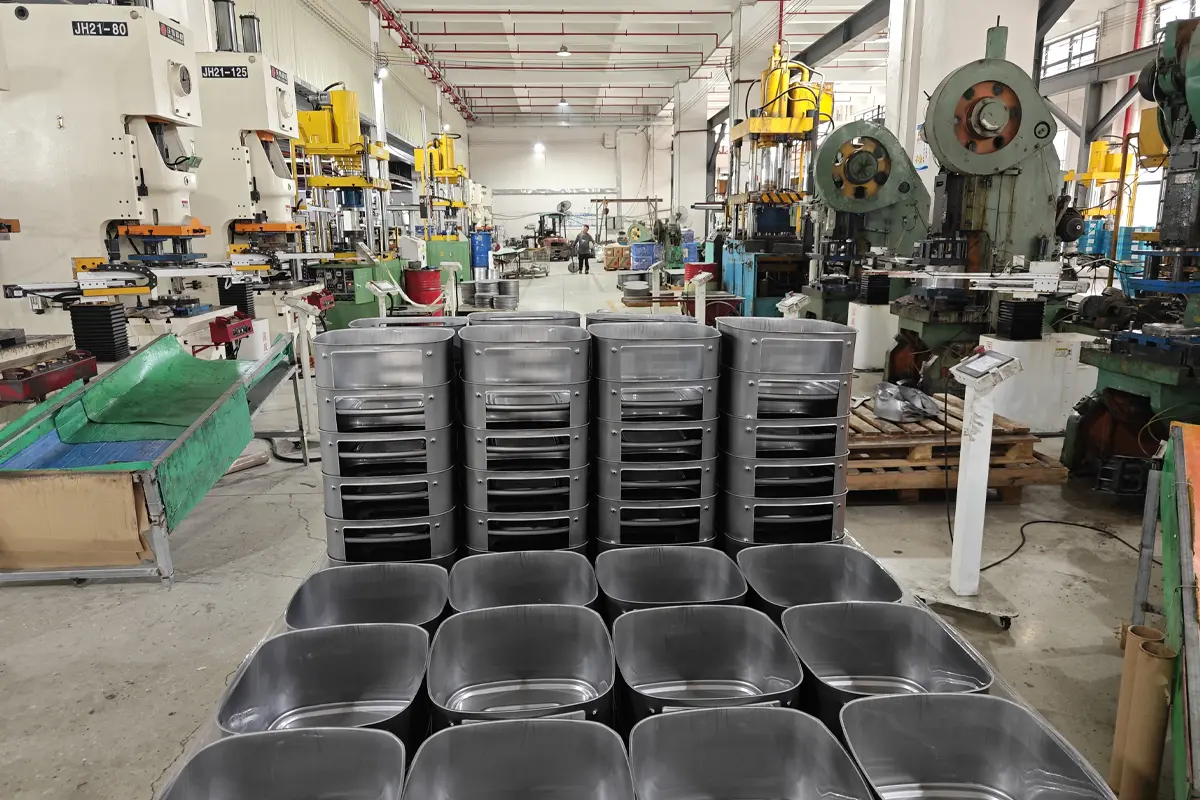
Semi-finished stamped parts need controlled handling so that shape, surface and batch separation are protected before the next process.
Questions Buyers Should Ask About Metal Stamping
A buyer does not need to become a stamping engineer to evaluate the workshop. But they should ask questions that connect metal processing with the finished appliance.
- Which metal parts are critical to assembly fit, user safety, coating or appearance?
- How are approved samples compared with production parts?
- What edge, surface and dimensional issues are checked before parts move forward?
- How are different models, versions and batches separated in the workshop?
- What happens if a stamped part fails first-piece or in-process review?
- How does the stamping workshop communicate with assembly and final inspection teams?
These questions are especially useful for private label and OEM/ODM projects, where even a small design change can affect tooling, forming behavior, assembly fit and finished product consistency.
Common Mistakes to Avoid
| Common mistake | Possible consequence | Recommended practice |
|---|---|---|
| Only approving the finished product sample. | Metal part issues may not be noticed until mass production. | Review critical metal parts during sampling and first article checks. |
| Ignoring edge and burr control. | Handling risk, coating problems or assembly rework. | Define acceptable edge condition and inspection method. |
| Changing metal thickness or shape without review. | Fit, strength, forming or cost may change unexpectedly. | Recheck tooling, sample parts and assembly fit after design changes. |
| Using vague drawing or sample references. | Factory and buyer may judge the part differently. | Keep approved drawings, photos, samples and defect examples aligned. |
| Allowing mixed semi-finished parts. | Wrong assembly, batch confusion and traceability difficulty. | Separate models, batches and versions clearly before assembly. |
Honest Advice
A metal stamping workshop is valuable only when it is connected to the full appliance production process. Equipment alone does not prove quality. Buyers should look at how material, tooling, first-piece review, semi-finished part handling, assembly feedback and final inspection work together.
How This Fits APEXDURA’s OEM/ODM Process
APEXDURA’s public production process includes demand analysis, mold R&D, material procurement, sample production and testing, metal stamping, injection molding, production, final testing, packaging, inspection, logistics and after-sales support. Metal stamping is therefore one step in a broader manufacturing route, not an isolated workshop.
For buyers planning OEM/ODM kitchen appliance projects, the practical value is early alignment. If a product requires a specific basket, bowl, support, panel, shell or bracket, that requirement should be discussed during the product brief, sample stage and production review. The production process and certificate information pages can help buyers prepare project questions before RFQ.
Explore More APEXDURA Workshop Capabilities
This metal stamping workshop is one part of APEXDURA's manufacturing flow. Buyers can also review our injection molding workshop, production assembly workshop and PCB soldering workshop to see how molded plastic parts, final assembly and control-board preparation connect with metal part production.
Limitations and Update Note
This article is a company capability introduction based on workshop photos taken in August 2026. It does not claim a fixed machine count, press tonnage, production capacity, defect rate, material grade, delivery time or certification coverage. Specific metal parts, materials, coatings, dimensions and inspection criteria depend on the product model, buyer specification and target market. Buyers should confirm project-specific requirements during RFQ and sampling.
Conclusion
Metal stamping may sit upstream from final assembly, but it has a direct effect on finished appliance quality. A stable metal part helps the product fit together, protects the intended appearance, supports coating or finishing, and reduces rework during assembly. A weakly controlled metal part can create visible gaps, sharp edges, deformation, mismatched holes or batch confusion later in the project.
For APEXDURA, the metal stamping workshop is part of an integrated OEM/ODM manufacturing process. For buyers, the key is to review metal components early, define clear acceptance criteria and connect stamping feedback with sampling, assembly and final inspection. That is how real workshop capability becomes practical sourcing confidence.
FAQ
What does a metal stamping workshop do for kitchen appliance production?
It forms sheet metal into appliance-related parts such as baskets, bowls, panels, brackets, shells or supports depending on product design and specification.
Why should OEM/ODM buyers care about metal stamping?
Metal part consistency can affect assembly fit, appearance, edge safety, coating quality and finished product reliability. It should be reviewed before mass production, not only after final assembly.
Do all APEXDURA product categories use the same stamped metal parts?
No. The part scope depends on each model. Air fryers, ovens, pressure cookers, microwaves, meat grinders and other kitchen appliances may use different metal structures and requirements.
Can buyers request custom metal parts?
Custom metal parts can be discussed as part of an OEM/ODM project. Tooling, material, shape, finish, inspection and target market requirements should be confirmed during the product brief and sampling stage.
Planning a kitchen appliance project with custom metal parts? Share your product category, part drawings or reference samples, target market, finishing requirements and expected inspection criteria with APEXDURA.
Contact APEXDURA to discuss metal part requirements for your appliance project