


Kitchen Appliance Pre-Shipment Inspection: 20 Checks
Kitchen Appliance Pre-Shipment Inspection: 20 Checks
A completed production order is not automatically ready for shipment. Kitchen appliances can pass assembly while still containing incorrect components, missing accessories, cosmetic defects, electrical failures, packaging errors, incorrect labels, or quantities that do not match the purchase order.
A kitchen appliance pre-shipment inspection verifies the actual finished order before the buyer releases the balance payment or authorises loading. This 20-point checklist helps importers turn a general instruction to “check the quality” into a documented shipment-release decision.
TL;DR — What the Inspection Must Confirm
A useful pre-shipment inspection should confirm five things:
- The finished products match the purchase order and approved sample.
- Safety-related and functional requirements have been verified.
- Quantities, accessories, labels, manuals, and packaging are correct.
- Defects have been classified under an agreed inspection plan.
- The order is complete, traceable, and ready for loading.
A factory capability review evaluates the supplier’s manufacturing system. A pre-shipment inspection evaluates the actual production lot being shipped.
Passing one does not replace the other.
Key Facts
AQL sampling is a lot-acceptance method, not a guarantee that every uninspected unit is defect-free.
The physical product must remain consistent with its approved model, electrical ratings, critical components, labels, manuals, and supporting conformity documents.
Critical safety defects should not be treated as ordinary cosmetic defects or accepted only because the overall AQL result passes.
A pre-shipment inspection does not replace accredited laboratory testing, conformity assessment, or the factory’s required production testing.
Pre-Shipment Inspection Is a Release Decision
A pre-shipment inspection should answer one commercial question:
Is this specific production lot acceptable for shipment under the agreed purchase order, approved sample, product specification, inspection criteria, and defect limits?
The inspector is not evaluating whether the factory looks modern or whether the showroom is impressive.
The inspector is comparing finished products with controlled references.
The inspection pack should include:
- Purchase order
- Approved product specification
- Approved golden sample
- Approved bill of materials where available
- Approved artwork
- Approved user manual
- Approved rating label
- Approved colour standard
- Approved packaging specification
- Carton and shipping marks
- Accessory list
- Inspection checklist
- Defect classification
- Agreed sampling plan
- Applicable functional tests
- Critical-component list
- Previous corrective actions
For private-label projects, these references should be approved before mass production. The private-label kitchen appliance launch guide explains how product specifications, packaging, certification, MOQ, and launch timing should be aligned before production starts.
Without controlled references, an inspector may identify visible defects but cannot reliably determine whether the order matches what the buyer approved.
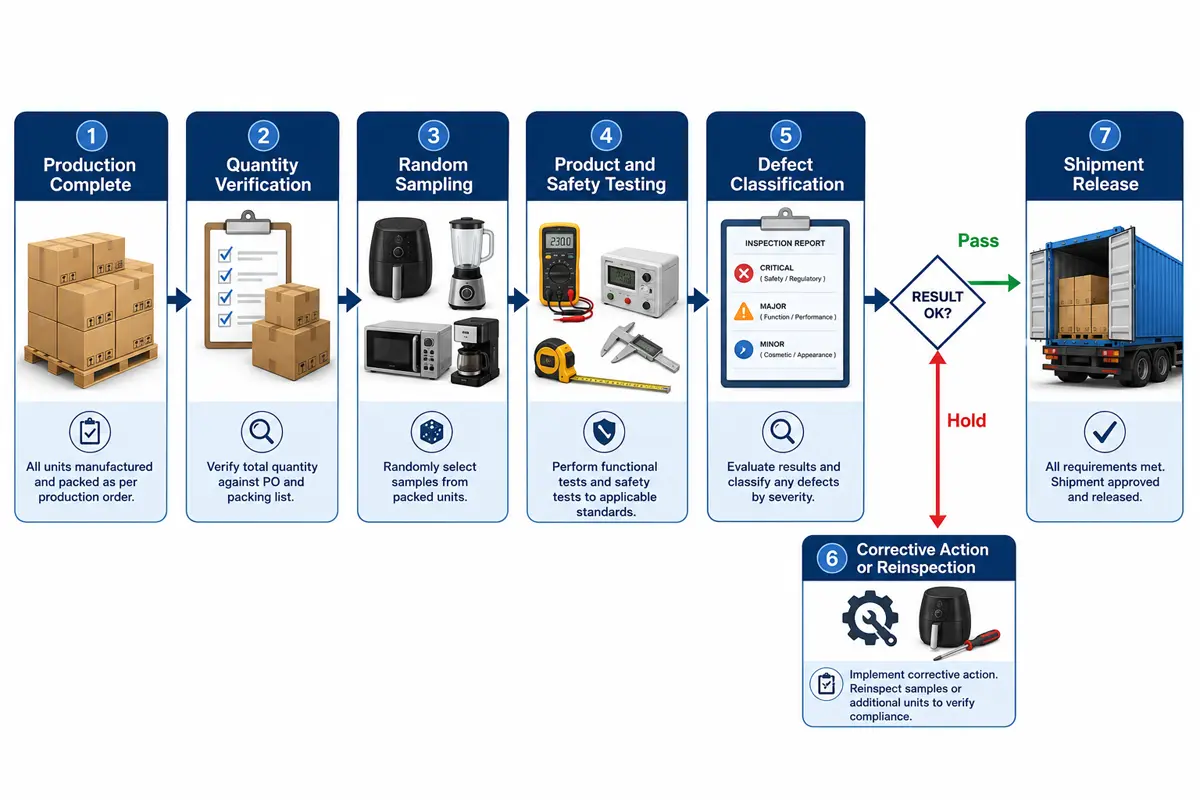
Shipment approval should follow evidence: production completion, random sampling, product checks, defect classification, corrective action, reinspection, and final release.
Check 1: Confirm That Production Is Substantially Complete
The inspection should normally take place after production is substantially complete and most units have been packed.
If too much production remains unfinished, the inspector is not evaluating the complete shipment. Units produced after the inspection may use different materials, workmanship, labels, accessories, firmware, or packaging.
Before scheduling the inspection, request:
- Total ordered quantity
- Total assembled quantity
- Total packed quantity
- Quantity awaiting rework
- Quantity still on the line
- Number of production batches
- Number of models and colours
- Voltage and plug breakdown
- Packaging-language breakdown
- Finished-goods warehouse location
The inspector should record the completion percentage and the number of units physically available.
Postpone the Inspection When:
- A significant portion of the order remains unfinished.
- Approved packaging has not arrived.
- The final firmware has not been installed.
- Important accessories are missing.
- Reworked units are mixed with accepted units.
- The factory cannot present the complete lot.
- Remaining production will use another component batch.
- Products are spread across uncontrolled storage locations.
Inspection timing should be coordinated with the confirmed manufacturing and shipping window. The production-slot planning guide for kitchen appliance importers explains how material arrival, assembly, packaging, inspection, and freight booking affect the final schedule.
Inspecting too early creates a false sense of control.
Check 2: Reconcile the Ordered Quantity
The inspector should compare the physical order with the purchase order and packing list.
Quantity should be checked by:
- Model
- Colour
- Rated voltage
- Plug type
- Language version
- Packaging version
- Accessory bundle
- Spare-parts quantity
- Replacement-unit quantity
- Master-carton quantity
Do not rely only on warehouse labels.
Selected cartons should be opened to confirm:
- Units per master carton
- Product configuration
- Colour and voltage
- Accessory quantity
- Manual language
- Retail-box version
Common quantity problems include:
- Mixed voltage versions
- Incorrect colour ratios
- Missing spare parts
- Wrong carton packing quantity
- Replacement units counted as commercial quantity
- Accessories stored separately
- Products allocated to another customer
- Unapproved overproduction
Check 3: Select Samples Randomly Across the Lot
The factory should not decide which cartons the inspector opens.
Samples should be selected from:
- Front, middle, and rear warehouse positions
- Upper and lower pallet levels
- Different production dates
- Different assembly lines where applicable
- Every model and colour
- Every voltage and plug version
- Different packaging-language versions
- Standard and reworked batches
The lot size, inspection level, sample size, AQL values, and acceptance or rejection numbers should be agreed before inspection.
Random sampling does not mean casually opening several convenient cartons.
The inspector should record where each sampled carton was selected.
Check 4: Compare the Product with the Approved Sample
The approved sample should be available during inspection.
Compare:
- Overall shape and appearance
- Dimensions
- Net weight
- Colour
- Surface texture
- Handle and control layout
- Product structure
- Basket, jar, lid, door, or inner cavity
- Accessories
- Display layout
- Button and knob function
- Logo size and position
- Rating label
- Warning labels
- Power cord and plug
- User interface
- Firmware version where applicable
A product can function correctly and still be commercially unacceptable because it does not match the buyer’s approved appearance or specification.
For OEM/ODM projects, logo, colour, packaging, control panel, plug, voltage, accessories, and firmware should be recorded through the APEXDURA OEM and ODM customisation process.
Warning — Sample Drift
Approval of one sample does not authorise later changes to:
- Motor
- Heating element
- Thermostat
- Thermal fuse
- PCB
- Display
- Power cord
- Plug
- Plastic material
- Coating
- Seal
- Firmware
- Packaging
- Critical sub-supplier
Any difference identified during inspection should be checked against an approved engineering or supplier-change record.
Where plastic parts are produced internally, mould revisions and raw-material control can affect consistency. The article on in-house injection moulding for kitchen appliance projects explains why tooling control matters after sample approval.
Check 5: Inspect Workmanship
Workmanship inspection covers visible and physical defects that affect appearance, assembly, use, saleability, or durability.
Typical checks include:
- Scratches
- Dents
- Cracks
- Stains
- Colour variation
- Injection marks
- Sink marks
- Sharp edges
- Loose screws
- Uneven gaps
- Poor panel alignment
- Damaged coatings
- Loose handles
- Unstable feet
- Excess glue
- Dirty surfaces
- Incorrect printing
- Missing markings
- Poor door or lid alignment
- Rattling components
- Poor accessory fit
The inspection specification should include photographs or measurable limits wherever possible.
Descriptions such as “good finish,” “normal gap,” or “acceptable appearance” are too subjective for consistent defect classification.
Check 6: Perform Product-Specific Functional Tests
Functional testing should reflect the actual product category and approved feature set.
Air Fryers and Electric Ovens
Check:
- Power-on
- Timer
- Temperature setting
- Heating operation
- Fan operation
- Basket or door interlock
- Control-panel response
- Display
- Abnormal noise
- Auto shut-off
- Internal light where applicable
- Accessories
- Visible smoke or unusual odour
Mechanical, digital, dual-basket, and oven-style products require different inspection points. The checklist should match the selected air fryer configuration or electric oven format.
Blenders and Juicers
Check:
- Power-on
- Speed settings
- Pulse function
- Jar or bowl interlock
- Motor sound
- Vibration
- Jar leakage
- Coupling engagement
- Blade rotation
- Lid fit
- Accessory fit
Motor performance, blade configuration, jar construction, coupling design, and safety interlocks should match the approved blender specification.
Coffee Machines
Check:
- Power-on
- Water flow
- Heating
- Pump operation
- Brewing
- Steam function where applicable
- Leakage
- Control-panel response
- Drip tray
- Removable water tank
- Cleaning function
- Error indication
Drip, espresso, capsule, and fully automatic coffee machine formats should not use the same generic functional checklist.
Electric Pressure Cookers
Check:
- Lid fit
- Lid locking
- Control panel
- Heating
- Menu selection
- Inner-pot fit
- Sealing ring
- Pressure-valve components
- Power cord
- Visible damage
- Error indication
The inspection must match the approved electric pressure cooker configuration, especially when the order includes customised menus, capacities, panels, or language versions.
Microwaves
Check:
- Door opening and closing
- Door-interlock response
- Control panel
- Turntable
- Interior light
- Timer
- Heating function
- Grill or convection function where applicable
- Abnormal noise
- Accessories
- Labels and warnings
Solo, grill, convection, mechanical, and digital microwave formats require different inspection points.
Functional testing during pre-shipment inspection does not replace complete product type testing or conformity assessment.
Check 7: Verify Routine Electrical-Safety Testing
Electrical appliances should be produced under a defined routine-test process.
Depending on product construction and applicable requirements, routine tests may include:
- Earth continuity
- Dielectric-strength testing
- Leakage-current testing
- Insulation checks
- Power-input verification
- Grounding verification
- Polarity or wiring checks
- Functional operation
During inspection, verify:
- Which tests were performed
- Whether every unit or only samples were tested
- Test limits
- Equipment identification
- Calibration status
- Production-test records
- Failed-unit records
- Repair records
- Reinspection after repair
The inspector should not conduct high-risk electrical tests without suitable equipment, procedures, and competence.
Routine production testing must remain consistent with the model’s conformity documentation. The CE certification guide for kitchen appliances explains the relationship between production checks, laboratory reports, the Declaration of Conformity, and the technical file.
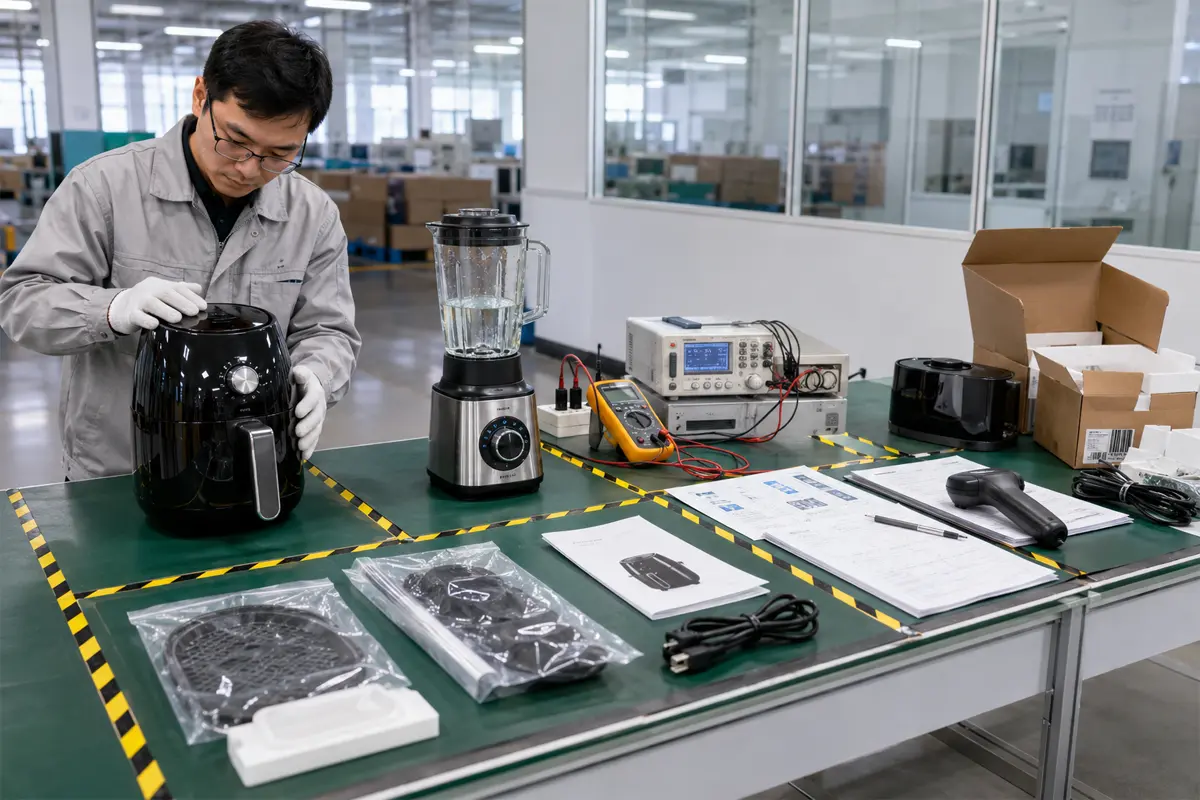
Finished-goods inspection must cover more than appearance. Function, electrical-test records, accessories, labels, manuals, and packaging all affect shipment approval.
Check 8: Verify Rating Labels and Product Identity
The physical product must match the approved and documented configuration.
Check the rating label for:
- Brand
- Model number
- Rated voltage
- Frequency
- Rated power
- Protection class
- Manufacturer identity
- Importer information where required
- Responsible economic-operator information where applicable
- Production or batch code
- Applicable conformity markings
- Disposal symbols
- Warning information
The model number and ratings should match:
- Purchase order
- Approved sample
- Product specification
- Test reports
- Declaration of Conformity
- User manual
- Packaging
- Technical documentation
A correctly printed CE mark does not correct a mismatch between the shipped product and its supporting documentation.
Material and environmental documentation should also be reviewed where applicable. The RoHS, REACH, and WEEE compliance guide explains the difference between restricted substances, chemical obligations, and electrical-product waste responsibilities.
Certification availability should always be confirmed by model and destination market through the APEXDURA certificates page.
Check 9: Review the User Manual
The user manual is a controlled product component.
Verify:
- Correct model
- Correct language
- Product illustration
- Electrical ratings
- Assembly instructions
- Operating instructions
- Cleaning instructions
- Safety warnings
- Food-contact guidance
- Disposal instructions
- Troubleshooting
- Warranty information
- Importer or responsible-party information where applicable
- App instructions for connected products
The manual must match the product actually being shipped.
Common errors include:
- Instructions copied from another model
- Functions shown that do not exist
- Incorrect voltage
- Incorrect accessories
- Missing local-language warnings
- Incorrect cleaning instructions
- Outdated control-panel artwork
- Outdated app screenshots
- Wrong product capacity
Check 10: Confirm Accessories and Spare Parts
Open sampled units and compare their contents with the approved accessory list.
Depending on the appliance, inspect:
- Cooking basket
- Crisper plate
- Rack
- Tray
- Jar
- Lid
- Blade
- Filter
- Measuring cup
- Cleaning tool
- Recipe book
- Power cord
- Adapter
- Spare seal
- Manual
- Warranty card
Accessories should be checked for:
- Correct quantity
- Correct material
- Correct colour
- Damage
- Fit
- Food-contact documentation where applicable
- Protective packaging
- Part number or identification
Spare parts supplied separately should be counted, identified, and packed separately from commercial finished goods.
Check 11: Scan Barcodes and Verify Retail Data
Incorrect barcode data can block an otherwise acceptable order at the retailer or warehouse.
Check:
- EAN or UPC
- Product model
- Product name
- Colour
- Voltage
- Unit quantity
- Master-carton quantity
- Country-of-origin information
- Gross weight
- Net weight
- Carton dimensions
- Shipping marks
- Pallet labels where applicable
Use a scanner rather than only reading the printed number.
Confirm that:
- The barcode scans successfully.
- The encoded number matches the approved artwork.
- Unit and master-carton barcodes differ where required.
- Different models and colours use the correct codes.
- Carton labels match the products packed inside.
- Retailer-specific labels are correctly positioned.
Check 12: Inspect Retail Packaging
Retail packaging should protect the product and communicate accurate information.
Inspect:
- Colour accuracy
- Print quality
- Printing position
- Product photography
- Model number
- Capacity
- Feature statements
- Conformity markings
- Warnings
- Language
- Barcode
- Product dimensions
- Accessory list
- Manufacturer details
- Importer information where applicable
- Carton damage
- Surface contamination
Treat unverified environmental, safety, health, performance, or certification claims as a commercial and compliance risk.
For private-label orders, the retail box, manual, rating label, barcode, warning label, and product sample should be approved as one controlled package rather than as unrelated files.
Check 13: Inspect Protective Packaging
Protective packaging should match the actual logistics and sales channel.
Check:
- Foam or moulded-pulp fit
- Polybag placement
- Scratch protection
- Accessory separation
- Cable protection
- Glass protection
- Product movement inside the box
- Carton closure
- Tape quality
- Corner protection
- Moisture protection
- Palletisation where applicable
Packaging designed for palletised retail distribution may not survive individual e-commerce parcel delivery.
The inspection standard should reflect whether the order is intended for:
- Palletised retail distribution
- Wholesale warehouse delivery
- Amazon fulfilment
- Direct-to-consumer parcel delivery
- Mixed-channel distribution
Packaging dimensions and protection levels should be reviewed together with the China-to-Europe kitchen appliance logistics plan, because carton size, CBM, container utilisation, freight mode, and warehouse handling affect landed cost and damage exposure.
Check 14: Measure Product and Carton Data
Measure sampled products and cartons instead of relying only on the supplier’s specification sheet.
Verify:
- Product dimensions
- Product net weight
- Gift-box dimensions
- Master-carton dimensions
- Gross weight
- Units per master carton
- Pallet quantity where applicable
- Container-loading calculation
Even a small increase in carton size can reduce container utilisation and increase landed cost.
Compare measured data with:
- Quotation
- Approved specification
- Packing list
- Shipping booking
- Retailer data sheet
- Warehouse master data
- E-commerce listing
Check 15: Verify Shipping Marks
Master-carton markings should match the approved format.
Check:
- Customer or consignee mark
- Purchase-order number
- Model number
- Colour
- Voltage
- Quantity
- Gross weight
- Net weight
- Carton dimensions
- Country of origin
- Carton number
- Handling symbols
- Barcode
- Batch identification
Incorrect shipping marks can create receiving and warehouse errors even when the product itself is acceptable.
Check 16: Test Batch Traceability
Select a finished product or carton and ask the factory to trace it back to:
- Production date
- Production line
- Shift
- Work order
- Batch number
- Critical-component batches
- Routine-test record
- Final-inspection record
- Packaging batch
Then perform the reverse check:
Select one critical-component batch and ask which finished-product batches used it.
Traceability should allow the supplier and importer to isolate an affected lot when a defect, complaint, corrective action, or recall occurs.
A traceability system that identifies only the production month may be insufficient for products produced across several lines, shifts, or component batches.
Check 17: Classify Defects Before Counting Them
The buyer should approve the defect-classification list before production.
Critical Defects
A critical defect creates or may create an unacceptable safety, legal, or compliance risk.
Examples can include:
- Exposed live electrical parts
- Failed grounding
- Dangerous sharp edge
- Unsafe wiring
- Failed safety interlock
- Wrong rated voltage
- Severe overheating
- Incorrect safety component
- Missing mandatory warning
- Incorrect compliance identity
- Microwave door-interlock failure
- Pressure-cooker lid-lock failure
- Pressure-protection failure
- Evidence of falsified records or markings
Critical defects should not be managed as ordinary cosmetic AQL defects.
A buyer may specify zero acceptance for defined critical defects, but the rule should be written into the inspection specification before production.
Major Defects
A major defect affects normal use, saleability, performance, durability, or required function.
Examples can include:
- Product does not operate
- Major accessory missing
- Significant leakage
- Damaged food-contact coating
- Incorrect control panel
- Wrong logo
- Unstable assembly
- Barcode failure
- Incorrect manual language
- Severe colour difference
- Loose handle
- Incorrect product feature
Minor Defects
A minor defect does not materially affect safety or normal use but reduces the quality of finish.
Examples can include:
- Small scratch
- Slight printing variation
- Minor gap variation
- Light packaging mark
- Small cosmetic mould mark
- Minor colour inconsistency
The same defect can have a different severity depending on:
- Location
- Product category
- Safety impact
- Retail channel
- Visibility
- Buyer specification
- Frequency across the sample
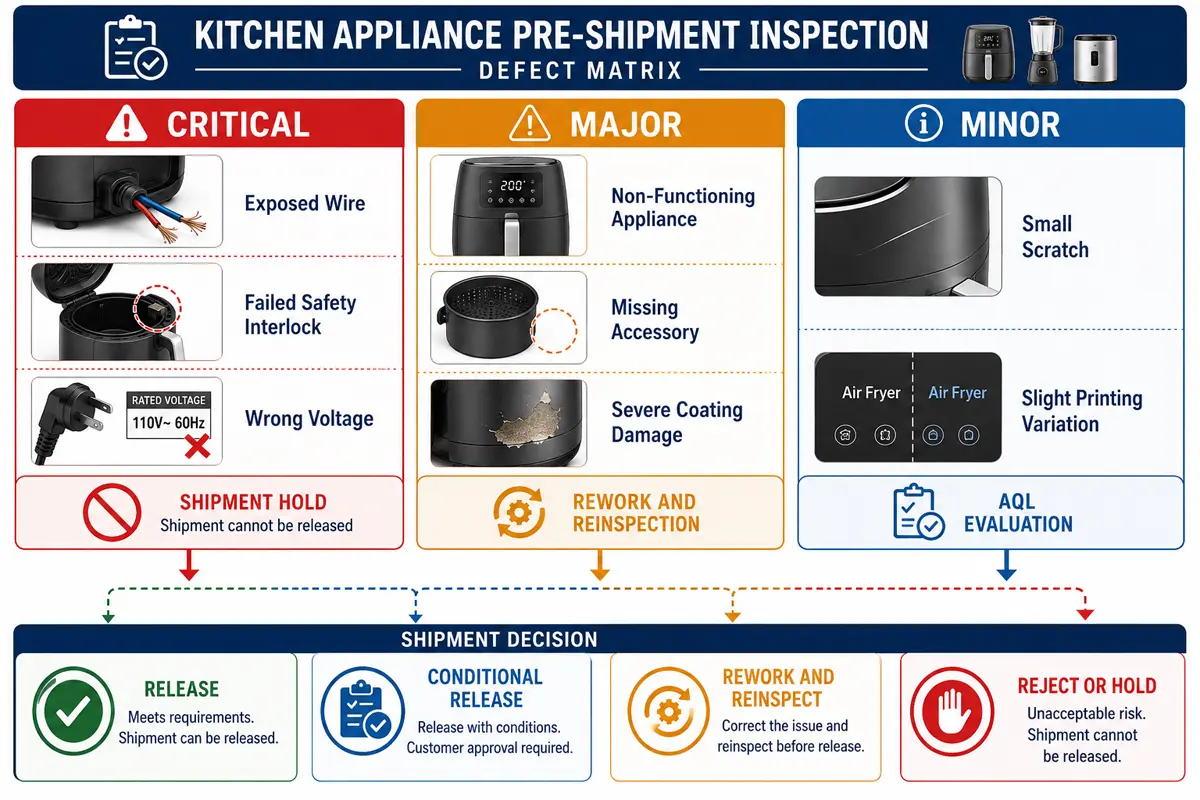
Critical defects require immediate escalation. Major and minor defects should be evaluated against the agreed sampling and acceptance plan.
Check 18: Apply the Agreed AQL Plan
AQL should be agreed in writing before the inspection.
The plan should state:
- Referenced sampling standard
- Lot definition
- Lot size
- Inspection level
- Sample-size code
- Sample size
- Critical-defect rule
- Major-defect AQL
- Minor-defect AQL
- Acceptance number
- Rejection number
- Functional-test sample size
- Destructive-test requirements
- Reinspection procedure
AQL does not mean the buyer agrees to receive a fixed percentage of defective products.
It is a statistical lot-acceptance method.
Honest Advice — AQL Is Not Suitable for Every Control
Some requirements should not rely only on ordinary random visual sampling.
Examples include:
- Mandatory production safety tests
- Correct voltage
- Correct plug version
- Required firmware
- Safety interlocks
- Legal product labels
- Product traceability
- Barcode data
- Critical safety components
- Approved power cord
- Approved thermal protection
These controls may require:
- 100% factory verification
- Production-test records
- Dedicated functional-test sampling
- Critical-component verification
- Separate laboratory testing
AQL should support the inspection plan, not replace product engineering and compliance controls.
Check 19: Require Complete Inspection Evidence
A useful report should contain:
- Supplier and factory details
- Purchase-order number
- Model and quantity
- Production-completion status
- Lot definition
- Sampling method
- Sample size
- Sample locations
- Defect photographs
- Defect counts
- Defect classification
- Functional-test results
- Measurement results
- Rating-label photographs
- Manual and barcode checks
- Packaging photographs
- Quantity reconciliation
- Traceability evidence
- Routine-test records reviewed
- Inspector comments
- Final result
Photographs should show context.
A close-up photograph of a scratch without identifying the product, position, model, and severity is insufficient for a commercial decision.
Check 20: Document the Shipment-Release Decision
The inspection result should lead to one of four documented decisions.
Release
Release the shipment when:
- Production is complete.
- Quantity is correct.
- Samples meet the agreed acceptance criteria.
- No unresolved critical defects exist.
- Products match approved specifications.
- Packaging and labels are correct.
- Traceability is available.
- Supporting documents are consistent.
Conditional Release
Conditional release may be considered when:
- The deviation is low risk.
- The buyer accepts it in writing.
- The commercial impact is understood.
- No safety or legal requirement is compromised.
- A formal concession is approved.
Conditional release should not be used for:
- Missing safety documentation
- Wrong voltage
- Failed safety interlock
- Unapproved critical component
- Incorrect product identity
- Missing traceability
- Falsified records
Rework and Reinspect
Use rework and reinspection when:
- The defect can be corrected.
- Affected products can be identified.
- The factory provides a controlled rework method.
- Reworked products are segregated.
- Reworked products are retested.
- A new random inspection can be performed.
Hold or Reject
Place the shipment on hold when:
- A critical defect is found.
- The wrong model or configuration was produced.
- Documents do not match the physical product.
- Quantity cannot be reconciled.
- Traceability is unavailable.
- Unapproved component changes are found.
- Rework cannot be controlled.
- The factory refuses corrective action.
- Evidence suggests document or product substitution.
The buyer or authorised buyer representative should retain final shipment-release authority.
20-Point Pre-Shipment Inspection Checklist
| # | Inspection Item | Evidence Required | Result |
|---|---|---|---|
| 1 | Production substantially complete | Completed and packed quantities | ☐ Pass ☐ Gap |
| 2 | Ordered quantity correct | Carton and unit reconciliation | ☐ Pass ☐ Gap |
| 3 | Samples randomly selected | Sampling record and locations | ☐ Pass ☐ Gap |
| 4 | Product matches approved sample | Side-by-side comparison | ☐ Pass ☐ Gap |
| 5 | Workmanship acceptable | Defect photographs and counts | ☐ Pass ☐ Gap |
| 6 | Functions operate correctly | Functional-test record | ☐ Pass ☐ Gap |
| 7 | Routine safety tests verified | Test and calibration records | ☐ Pass ☐ Gap |
| 8 | Rating labels correct | Label and document comparison | ☐ Pass ☐ Gap |
| 9 | User manuals correct | Model and language review | ☐ Pass ☐ Gap |
| 10 | Accessories complete | Accessory-list comparison | ☐ Pass ☐ Gap |
| 11 | Barcodes scan correctly | Scanner results | ☐ Pass ☐ Gap |
| 12 | Retail packaging approved | Artwork comparison | ☐ Pass ☐ Gap |
| 13 | Protective packaging adequate | Packaging-method review | ☐ Pass ☐ Gap |
| 14 | Product and carton data correct | Measurements and weights | ☐ Pass ☐ Gap |
| 15 | Shipping marks correct | Carton photographs | ☐ Pass ☐ Gap |
| 16 | Batch traceability available | Production and test records | ☐ Pass ☐ Gap |
| 17 | Defects classified correctly | Approved defect list | ☐ Pass ☐ Gap |
| 18 | Sampling plan correctly applied | AQL plan and result | ☐ Pass ☐ Gap |
| 19 | Inspection evidence complete | Full report and photographs | ☐ Pass ☐ Gap |
| 20 | Release decision documented | Release, rework, hold, or reject | ☐ Pass ☐ Gap |
Red Flags That Override the AQL Result
Do not approve shipment only because defect totals are below the AQL rejection number.
Place the shipment on hold when any of these conditions occurs:
- Critical safety defect
- Incorrect rated voltage
- Incorrect plug configuration
- Product identity does not match documents
- Unapproved safety-component change
- Routine electrical-test records are unavailable
- Products cannot be traced
- Mandatory warnings are missing
- Factory-selected samples are presented as random samples
- A large portion of the order is unavailable
- Reworked products are mixed with accepted products
- Inspection or test records appear falsified
- The factory refuses access to finished goods
- The production location differs from the declared factory
From APEXDURA’s Quality Desk
Pre-shipment inspections produce better decisions when the inspection specification is completed before mass production begins.
Buyers who define the approved sample, critical components, test methods, defect classification, artwork, accessories, packaging, traceability, and release rules before production are less likely to face subjective arguments at final inspection.
A request to “check quality before shipment” is too broad.
A controlled inspection plan converts quality expectations into measurable acceptance criteria.
Review how incoming materials, assembly, production testing, final inspection, packaging, traceability, and shipment preparation are managed through the APEXDURA production process.
Frequently Asked Questions
When should a kitchen appliance pre-shipment inspection take place?
A pre-shipment inspection should normally take place after production is substantially complete and most units have been packed, but before the goods are loaded or the final balance is released.
Inspecting too early leaves part of the production order outside the verified lot.
Does passing an AQL inspection guarantee that every product is defect-free?
No.
AQL inspection uses random sampling to support an acceptance or rejection decision about a production lot. It does not inspect every unit and does not guarantee that every uninspected unit is defect-free.
What AQL level should be used for kitchen appliances?
The correct AQL values depend on product risk, buyer requirements, retail channel, supplier performance, defect classification, and the inspection agreement.
Critical safety defects should be managed separately from normal major and minor workmanship defects.
The AQL plan must be approved before inspection, not selected after defects have been found.
Should electrical safety be checked during pre-shipment inspection?
Yes, but the scope must be controlled.
The inspection should verify relevant production-test records, equipment calibration, failed-unit controls, and selected safety-related checks where appropriate.
Pre-shipment inspection does not replace accredited laboratory testing, conformity assessment, or required factory routine testing.
Can the factory perform its own final inspection?
Yes.
The factory can conduct its own final inspection, but buyers may use their own inspectors or an independent inspection company for first orders, private-label programmes, higher-risk products, large orders, or major retail projects.
The inspector should follow the buyer’s approved specification rather than relying only on the factory’s internal standard.
What happens if an order fails inspection?
The buyer should place the shipment on hold and review the defect evidence.
The factory should provide:
- Containment action
- Affected quantity
- Root-cause analysis
- Rework method
- Retesting plan
- Completion date
- Reinspection request
A new inspection should verify the corrected order before shipment.
The commercial consequences should already be defined in the purchase agreement. The MOQ and payment-terms guide explains how inspection approval can be connected to final payment and shipment release.
Ready to define your appliance inspection requirements before shipment?
Send us your product category, target market, order quantity, packaging requirements, and inspection standard. We will confirm the relevant product specifications, testing records, packaging details, and inspection arrangements.
Submit your inspection and OEM/ODM requirements →
Source Inspection-Ready Kitchen Appliances with APEXDURA
APEXDURA is the international brand of Zhongshan Zhenmei Electrical Appliance Co., Ltd., with 16 years of OEM/ODM manufacturing experience, annual output of 500,000 units, a 0.8% defect rate, and 12 production lines.
- Approved-sample and product-specification control for OEM/ODM orders
- Packaging, manual, label, barcode, and accessory approval
- Functional and production-test records confirmed by model
- Buyer-defined defect classification and inspection support
- Batch traceability and corrective-action coordination
- Rework and reinspection support before shipment release
Documentation, test-report status, and inspection availability are confirmed according to the product model, destination market, and purchase-order requirements.
Every enquiry receives a response within 24 hours.
Email: devin@zszhenmei.com
WhatsApp: +86 136 1272 5240