


Second Supplier Strategy: Why Kitchen Appliance Brands Need a Backup Manufacturing Partner
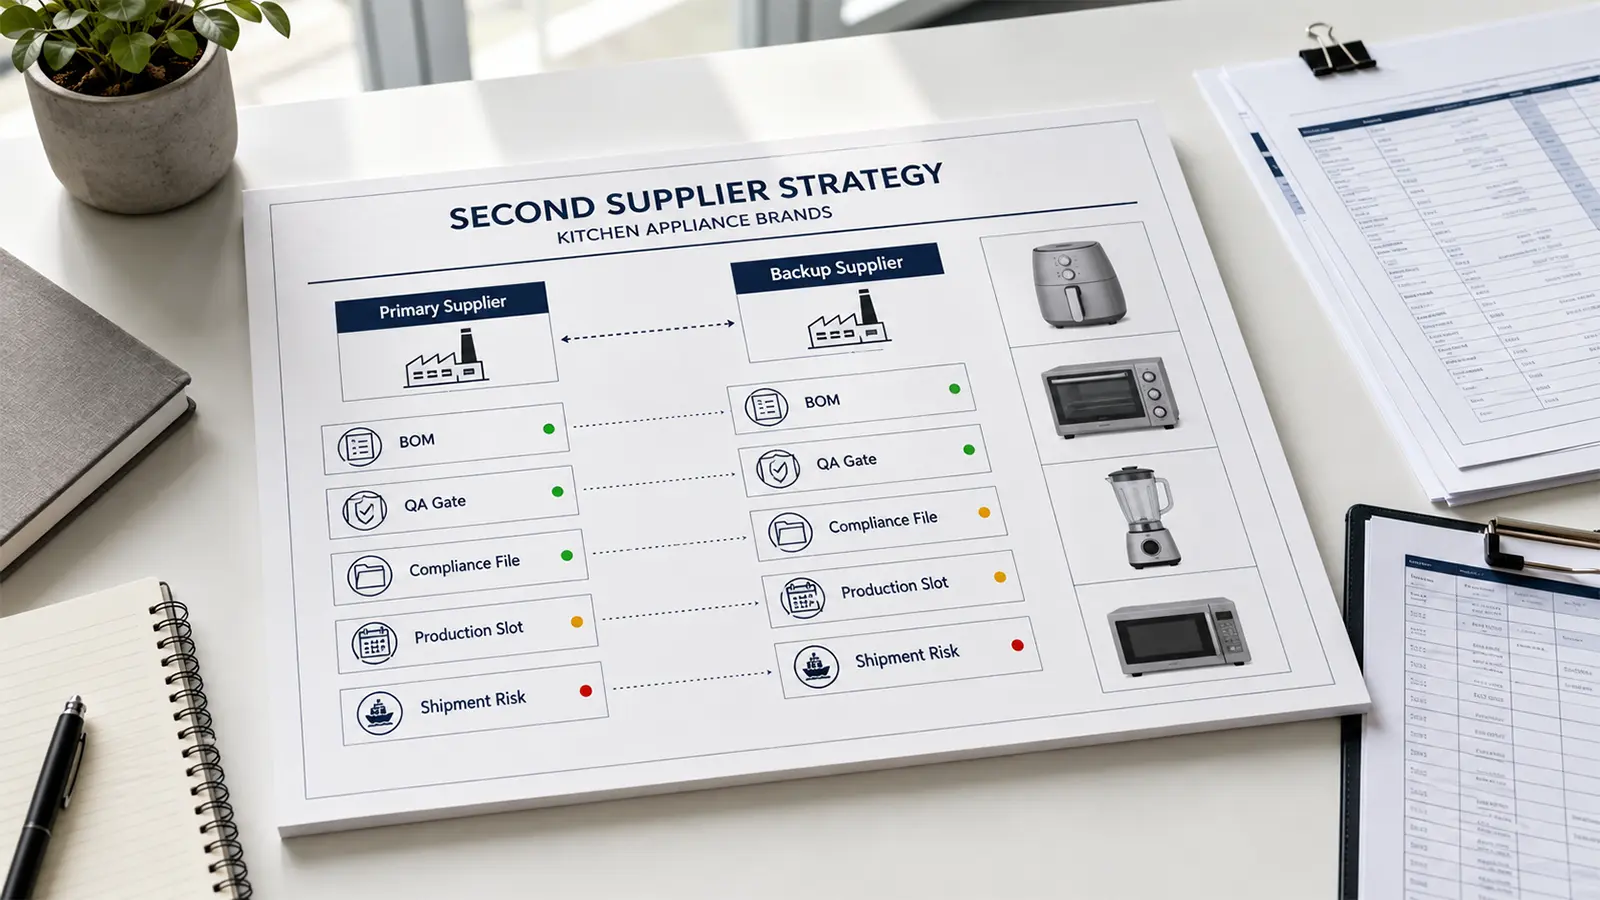
A second supplier strategy helps kitchen appliance brands reduce supply risk, but it is not simply about finding another factory. The real work is deciding which SKUs need backup capacity, aligning specifications, qualifying samples, comparing compliance evidence and setting clear rules for volume allocation before disruption appears.
Quick Answer: When Does a Second Supplier Make Sense?
Use a second supplier when one approved manufacturing partner has become a business continuity risk for a critical SKU. That risk may come from capacity, key components, compliance documentation, quality drift, limited product-development support, long response times or heavy dependence on one production route.
Do not use a second supplier only as a last-minute price weapon. If the second factory receives unclear drawings, a moving BOM and no agreed inspection standard, the buyer may get two different versions of the same product and double the management workload.
For kitchen appliances, the stakes are practical. An air fryer, oven, blender, microwave or electric pressure cooker is not only a plastic housing and a price quote. It includes electrical safety, food-contact surfaces, control panels, packaging, labels, manuals, spare parts expectations and market-specific compliance files. A backup manufacturing partner has to match the product intent, not just the outer appearance.
Key Takeaways
- A second supplier is most valuable for critical SKUs with real continuity risk, not every low-volume product.
- The qualification process should compare evidence, sample performance and production readiness before splitting volume.
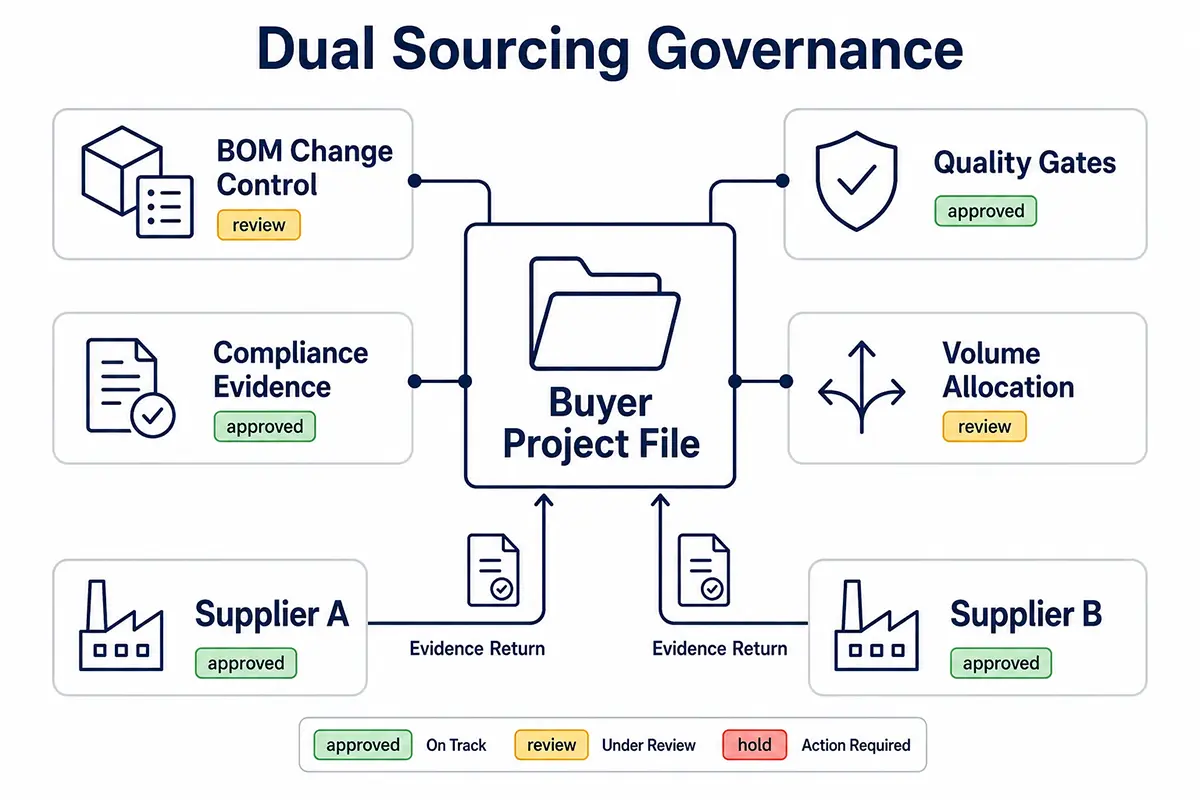
- BOM control is the center of dual sourcing. Without an agreed BOM and change-approval rule, two suppliers can quietly create two product versions.
- Quality gates should include sample approval, first production checks, AQL plans and pre-shipment inspection, not only a factory profile.
- The commercial benefit appears when the buyer can maintain supply options without losing technical, compliance and packaging consistency.
Five Risk Triggers That Justify a Backup Manufacturer
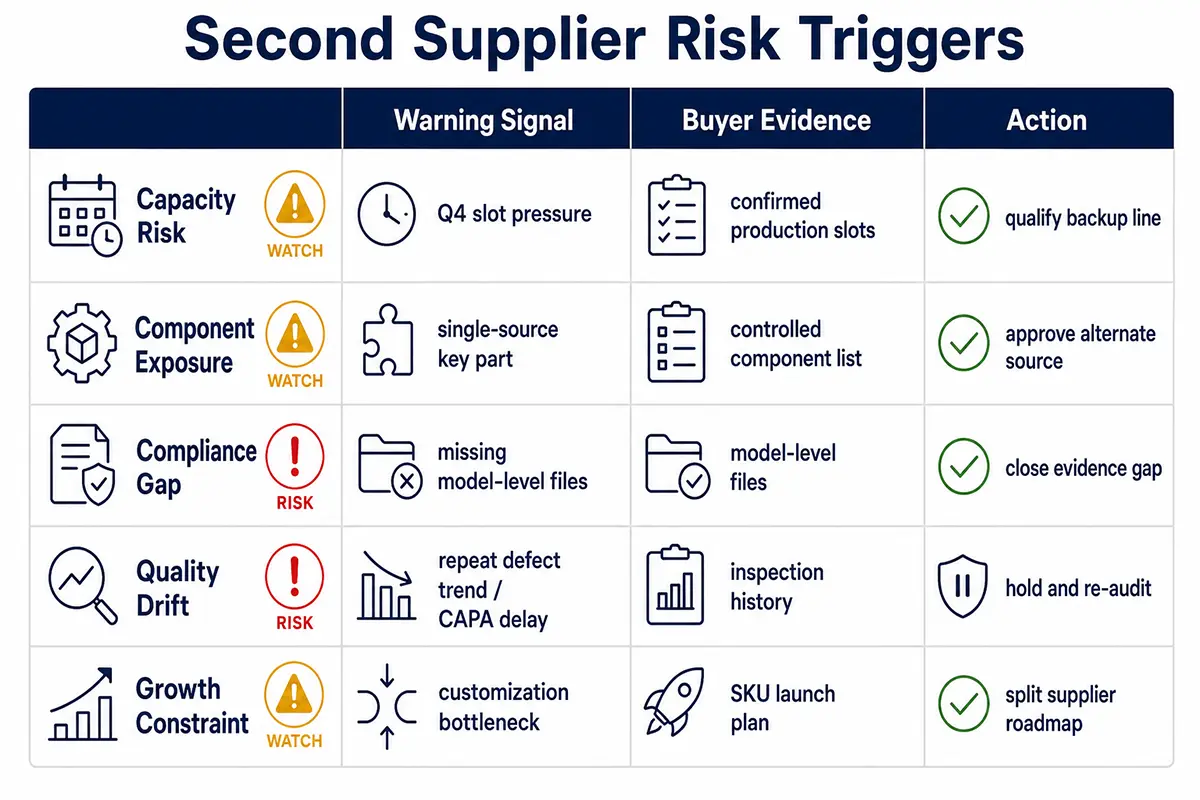
Supply-chain risk work should start by mapping known risks and monitoring them over time. For appliance buyers, that means turning vague anxiety into a visible supplier risk register. The table below gives a practical first filter.
| Risk Trigger | What It Looks Like | Second Supplier Action |
|---|---|---|
| Capacity or seasonal slot risk | The current factory is strong but Q4 slots, tooling bandwidth or packaging capacity are repeatedly tight. | Qualify a backup supplier for the same SKU or a secondary SKU family before seasonal orders are locked. Use a production slot planning review to set the trigger date. |
| Critical component exposure | One heater, motor, PCB, coating, jar, pressure component or controller drives a large share of risk. | Ask both suppliers to identify controlled components, approved alternatives and change-notification rules. Link this to component traceability. |
| Compliance evidence gaps | The supplier can sell the product but cannot provide model-level test reports, DoC support, material declarations or user-instruction evidence in a consistent way. | Use the second supplier qualification as a compliance-file comparison, especially for CE, RoHS, LFGB or other requirements confirmed by model and market. |
| Quality or response drift | Defect trends, late corrective actions, unclear root cause reports or repeated packaging issues are becoming normal. | Do not move immediately to volume. First create a corrective-action threshold and qualify another supplier through sample, pilot and inspection gates. |
| Strategic growth constraint | The brand wants a wider product range, new packaging, UI customization or faster development than the current partner can support. | Screen a second supplier for development depth, engineering communication and OEM/ODM fit, not only unit price. |
Qualification Gates: Do Not Split Volume Too Early
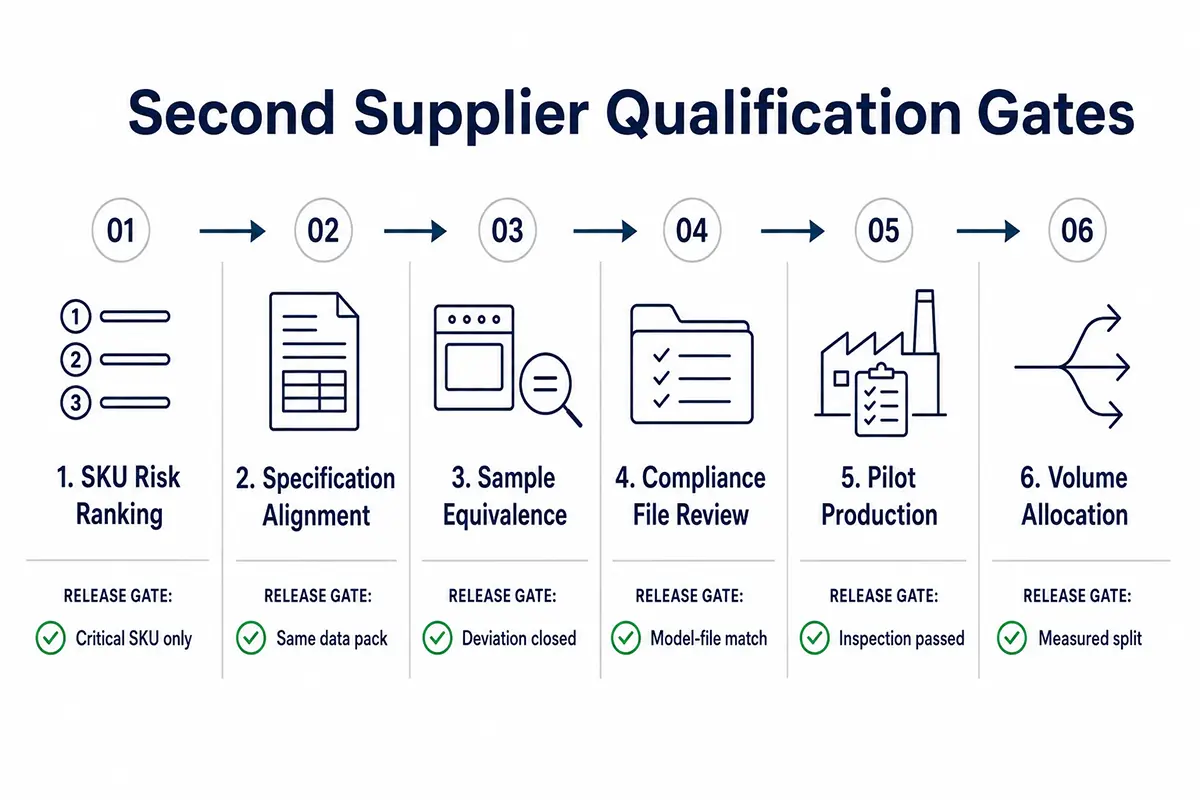
A second supplier should move through staged gates. The point is not to prove that another factory can make something that looks similar in a showroom. The point is to prove that it can repeat the agreed version under production conditions, with documented controls.
| Gate | Buyer Action | Supplier Evidence | Release Decision |
|---|---|---|---|
| 1. SKU risk ranking | Choose which products need backup first. | Annual forecast range, margin importance, market coverage, current supplier risk notes. | Only critical or growing SKUs enter qualification. |
| 2. Specification alignment | Freeze target product definition before quoting. | Specification sheet, BOM version, packaging files, manual language needs, target market notes. | No quote comparison until requirements are comparable. |
| 3. Sample equivalence | Compare function, user experience, structure and safety-related design details. | Sample report, photos, deviation list, material and component notes. | Approve, revise or reject before pilot order. |
| 4. Compliance file review | Check whether documents match the actual model and target market. | Test report scope, declaration support, RoHS or material evidence, food-contact evidence where applicable, user instructions. | Proceed only when gaps are understood and assigned. |
| 5. Pilot production | Run a small controlled order or first-production review. | First article records, line setup, inspection plan, packaging check, corrective-action record. | Move to conditional approval if deviations are closed. |
| 6. Volume allocation | Set the split based on risk and readiness. | On-time delivery, defect trend, responsiveness, documentation discipline, cost stability. | Use a measured allocation, not an emotional switch. |
If the project is still at sample stage, use first article inspection thinking early. If the order is moving toward shipment, align the backup supplier's criteria with the buyer's AQL sampling and pre-shipment inspection expectations. Otherwise, Supplier A and Supplier B may pass different versions of the same requirement.
The RFQ Data Pack Your Second Supplier Needs
Many second supplier projects fail before the first quote because the buyer sends an old sample, a short photo brief or an incomplete RFQ. The receiving factory then estimates, substitutes or designs around missing information. That can be useful for early exploration, but it is risky when the buyer expects a true backup version.
| Data Pack Item | Why It Matters | Buyer Note |
|---|---|---|
| Target product and use case | Clarifies whether the product is an entry model, premium SKU, promotion item or channel-specific version. | Include target market, user scenario and retail channel. |
| Approved sample or reference specification | Gives the second supplier a baseline for size, function, interface and packaging intent. | Mark what must match and what can be redesigned. |
| BOM version and controlled components | Prevents quiet changes in heater, motor, PCB, coating, jar, seal, plug or packaging material. | Define which alternatives require buyer approval. |
| Target certifications and documents | Links the model to CE, RoHS, LFGB, CB, ETL or other requirements where applicable. | Do not ask for "all certificates"; ask what applies to the specific model and market. |
| Inspection and defect criteria | Allows the supplier to quote with the real quality expectation in mind. | Include major defects, critical safety checks and packaging acceptance rules. |
| Customization scope | Logo, panel language, color, finish, plug, gift box and accessories may change tooling, MOQ, evidence and timing. | Separate must-have customization from optional upgrades. |
Lead magnet idea for CMS: offer a downloadable "Second Supplier Readiness Scorecard" PDF and a short online self-check form. Suggested fields: product category, target market, annual forecast range, current supplier pain point, BOM status, required certificates, sample availability, packaging language, target launch window and decision owner.
This gives procurement readers a useful tool in the middle of the article instead of waiting until the final paragraph to invite contact.
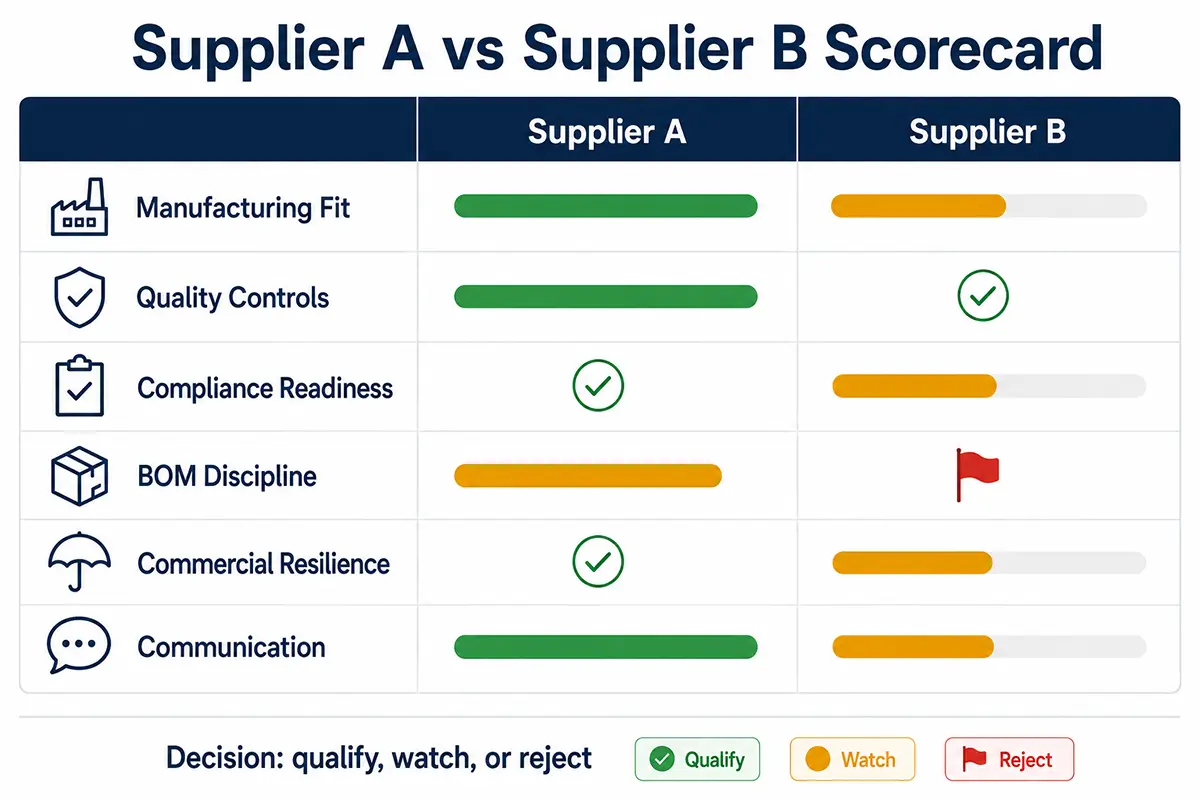
A Practical Scorecard for Comparing Supplier A and Supplier B
A second supplier should not be evaluated only on FOB price. Price matters, but a lower quote can be misleading if it creates more incoming inspection, unclear documentation, rework, slow corrective action or different packaging results.
| Evaluation Area | What to Compare | Strong Signal | Weak Signal |
|---|---|---|---|
| Manufacturing fit | Product category experience, process match, customization capability. | Supplier understands the appliance type and can explain key production risks. | Supplier only says "we can make it" without process details. |
| Quality controls | Incoming materials, line checks, final testing, inspection records. | Controls are tied to the product and buyer acceptance criteria. | Quality is described only as "strict inspection". |
| Compliance readiness | Model-level evidence, material files, user instructions, label support. | The supplier states which documents are available and which require project confirmation. | Generic certificate lists are sent without model scope. |
| BOM discipline | Version control, substitution approval, traceability and change notification. | Controlled parts and alternatives are recorded before production. | Substitution decisions are left to purchasing without buyer sign-off. |
| Commercial resilience | Capacity, MOQ, payment terms, seasonal scheduling, packaging support. | Terms are realistic and linked to forecast, SKU complexity and schedule. | The offer is attractive but the supplier cannot explain constraints. |
| Communication | Technical response speed, deviation reporting, English documentation, meeting discipline. | Open issues are tracked with owner, date and next action. | Responses are fast but vague, or every issue is marked "no problem". |
For OEM/ODM kitchen appliance projects, the most useful second supplier discussion starts with the buyer's risk profile, not a generic catalogue request. APEXDURA can review product category, target market, customization scope, required evidence and expected order rhythm, then discuss whether an existing platform, modified ODM model or deeper OEM project is a better fit. Certifications and documents should always be confirmed by model and target market at RFQ stage.
APEXDURA supports OEM/ODM kitchen appliance projects across categories such as oven, air fryer, blender, microwave, electric pressure cooker, coffee machine, juicer and meat grinder. Buyers can use the OEM/ODM service page to frame customization needs and the production process page to understand how project communication, materials, samples, production, testing, packaging and inspection connect.
How to Set Volume Split Without Damaging Quality
There is no universal split. A buyer may start with a small pilot at the second supplier, keep the main volume with the primary supplier, and increase the backup share only when performance records justify it. The important point is to connect allocation to evidence.
| Situation | Recommended Split Logic | Governance Rule |
|---|---|---|
| First qualification order | Small pilot volume only. | No promotion launch depends on the second supplier until pilot issues are closed. |
| Seasonal capacity backup | Primary supplier remains main source; second supplier receives pre-defined overflow or non-critical SKU volume. | Trigger is tied to slot pressure, material readiness or confirmed demand increase. |
| Strategic dual sourcing | Measured split based on performance, forecast, region and product family. | Both suppliers follow the same approved specification, inspection criteria and change-control rules. |
| Emergency shift | Move only the SKU and quantity that the second supplier has already qualified for. | Emergency volume still requires compliance and quality release. Do not skip evidence because the date is tight. |
Common Mistakes and Red Flags
| Mistake | Why It Hurts | Better Practice |
|---|---|---|
| Using the second supplier only to push the primary supplier's price down. | It creates distrust and often produces shallow quotes instead of real readiness. | Define the risk problem first: capacity, quality, compliance, product development or continuity. |
| Sending an old sample without an approved data pack. | The second supplier may copy appearance but miss material, electrical, packaging or document requirements. | Send controlled specifications and mark which features must match. |
| Approving samples but skipping pilot production checks. | Sample-room quality may not match line output, especially for customized panels, coatings, assemblies or packaging. | Use a first production review before approving meaningful volume. |
| Comparing certificates without checking model scope. | Documents may apply to another variant, market or component configuration. | Use the certificate information as a starting point, then confirm exact model scope at RFQ stage. |
| Letting two suppliers change components independently. | The buyer ends up managing two versions of one SKU, which complicates service, compliance and repeat orders. | Set a written change-approval rule and maintain a shared controlled-component list. |
Honest Advice: When a Second Supplier Is Not the Right Move
A second supplier is not always worth the management cost. If the product is low volume, the current supplier is stable, the tooling is highly customized, the brand has not frozen specifications, or the buyer cannot manage two document streams, a second supplier may add confusion before it adds resilience.
In those cases, a better first step may be to strengthen the current supplier controls: clearer BOM freeze rules, better production-slot planning, stronger pre-shipment inspection criteria, more disciplined corrective-action follow-up and a realistic risk review before peak season. After that foundation exists, the buyer can decide whether a backup manufacturing partner is still necessary.
Illustrative Scenario: The Q4 Air Fryer Oven Launch
A European private-label brand plans a Q4 air fryer oven promotion. The primary supplier made the approved sample, but the buyer sees three warning signs: seasonal production slots are filling, the heating element has a long material lead time, and the packaging file is still changing. Instead of waiting for a crisis, the buyer starts a second supplier review in August.
The buyer sends a controlled data pack, asks for a deviation list, checks model-level compliance evidence, requests a pilot order plan and agrees that the second supplier will not receive promotional volume until sample equivalence and first production evidence are reviewed. The result is not a dramatic factory switch. It is a safer option: if the primary supplier stays on track, the second supplier remains qualified for overflow or the next SKU. If a real disruption appears, the buyer already knows what the second supplier can and cannot handle.
Limitations and Update Note
This guide was last reviewed on August 15, 2026. It is a sourcing and manufacturing decision guide, not legal, tax, customs or contract advice. Exact supplier qualification steps depend on product category, tooling ownership, target market, compliance scope, order quantity, material readiness and the buyer's internal risk tolerance.
Certification types, test reports and technical documentation must be confirmed by model and target market. APEXDURA does not present certification as universal across all models or markets. Buyers should check the specific product configuration, intended use, packaging, labels, user instructions and applicable regulatory requirements before placing an order.
Final Takeaway
A second supplier strategy is strongest when it is boring in the right way: documented, staged, measurable and reviewed before pressure appears. The goal is not to replace one factory with another overnight. The goal is to give the buyer a controlled option for continuity, capacity, quality and product-development flexibility.
If your brand is reviewing backup manufacturing options for air fryers, ovens, blenders, microwaves, electric pressure cookers, coffee machines, juicers or meat grinders, prepare a short risk brief first. Include your product category, target market, expected annual quantity, current supplier risk, BOM status, customization needs and required evidence. Then contact APEXDURA to discuss whether a second supplier review, ODM alternative or OEM project assessment is the right next step.